

Powder Enamel Gun
For Glass Frit. Wear-Resistant.
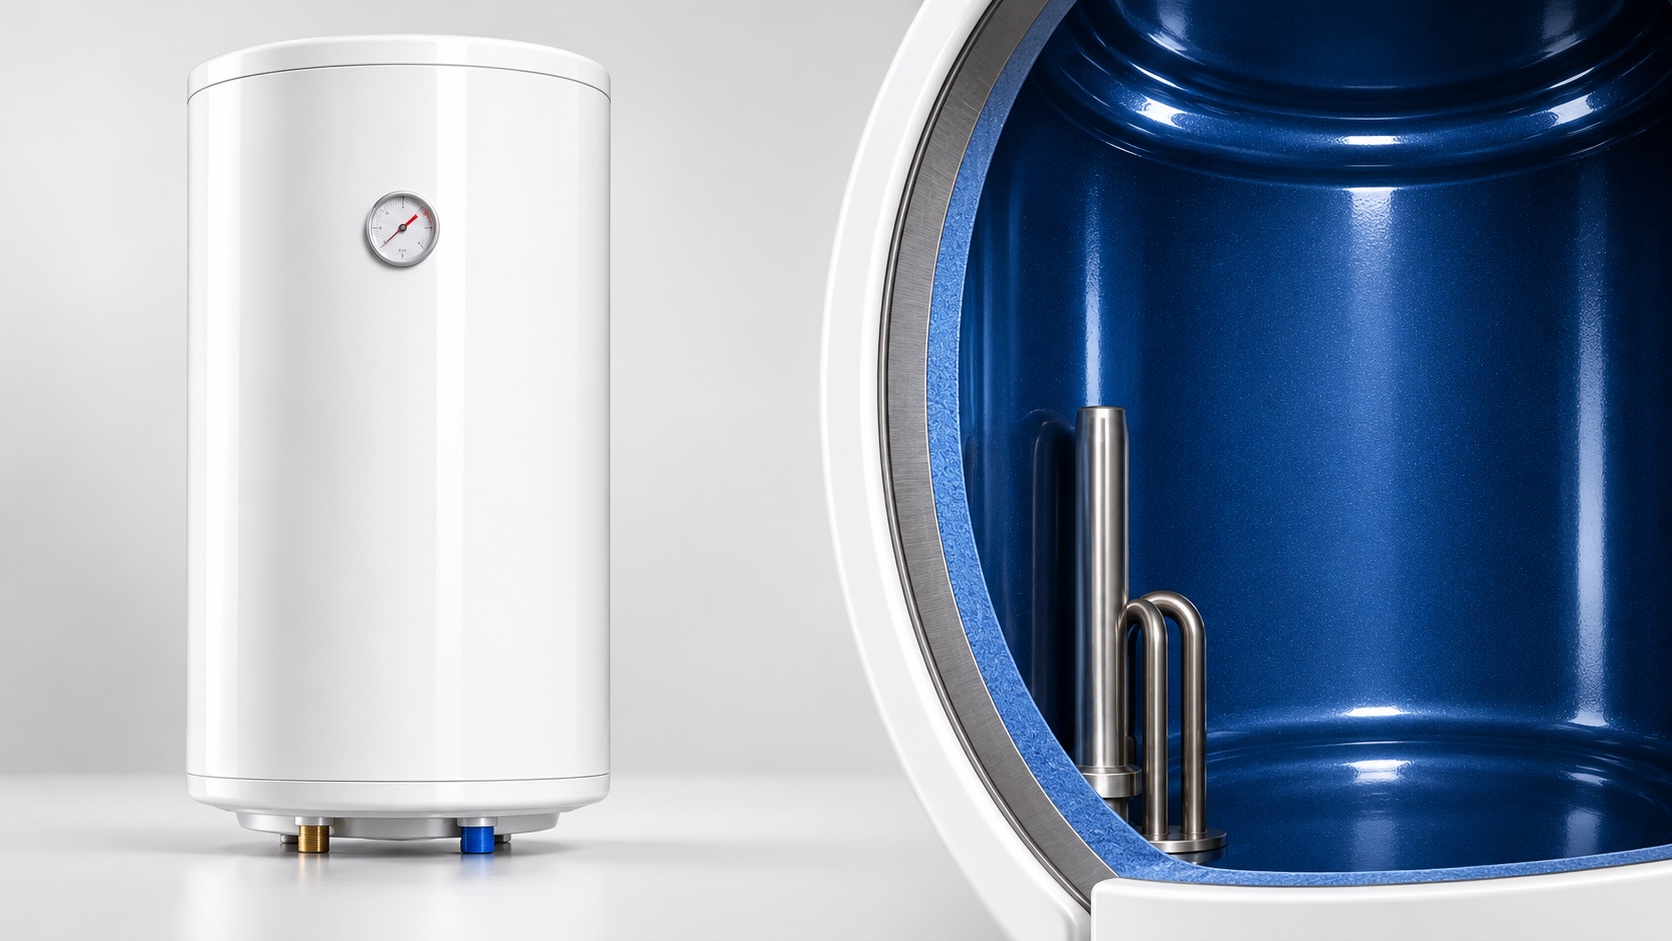
The Powder Enamel Gun is engineered to apply electrostatic dry glass-frit enamel powder. Enamel is glass — not paint: it is finely milled glass frit, surface-treated so it can hold an electrostatic charge, and it is fired at roughly 780–850°C to fuse into a glass layer on the metal. Because this frit is far more abrasive than organic powder paint, the gun runs a wear-resistant powder path and charging characteristics tuned for enamel frit, delivering a consistent, clean coat on steel panels, oven cavities and water-heater/boiler tanks.
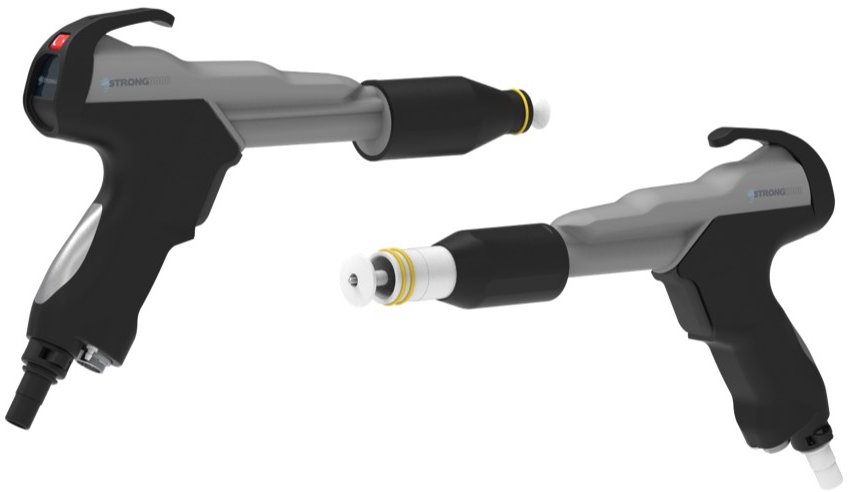
Enamel Is Glass — Not Paint.
Powder enamel is dry glass frit that is electrostatically charged, applied to metal and then fired at high temperature to become glass. Organic powder coating is a polymer film cured at roughly 160–200°C; powder enamel is an inorganic glass coating that melts and fuses to the metal at roughly 780–850°C. The two processes are chemically different, and enamel should never be called paint.
Because glass frit is hard and abrasive, it quickly wears the internal path of a standard powder coating gun. This gun answers that with a powder channel built from wear-resistant materials and charging settings optimized for enamel frit, suited to steel panels, oven cavities and tanks that demand chemical resistance and heat durability.
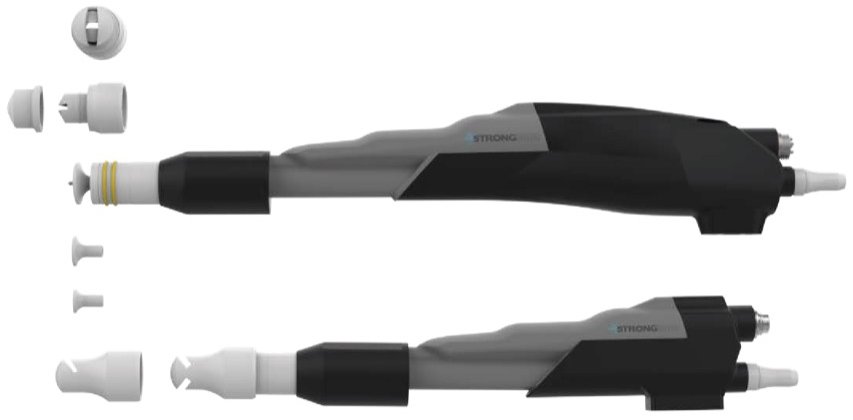
Engineered for Glass Frit.
Wear-Resistant Powder Path
Powder channel and components protected against abrasive frit.
Charging Tuned for Enamel
Electrostatics optimized for surface-treated frit to hold charge.
High-Temperature Coating
Glass coating fused to metal by firing at ~780–850°C.
Industrial Use
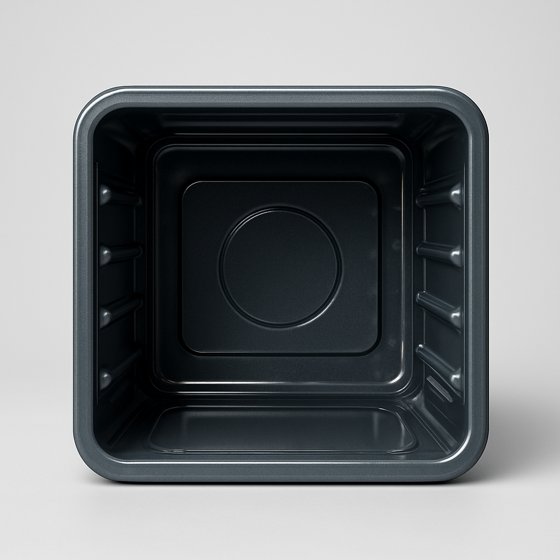
Steel panels, oven cavities and water-heater/boiler tanks.
Take a Closer Look.
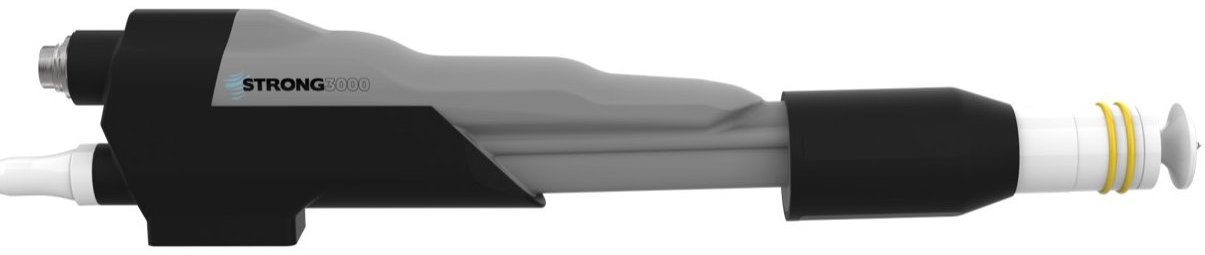
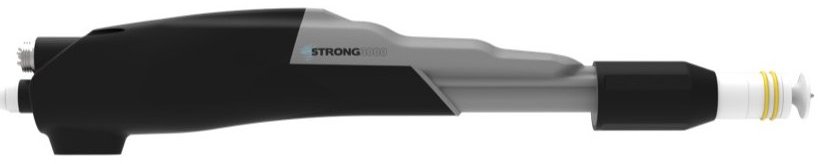
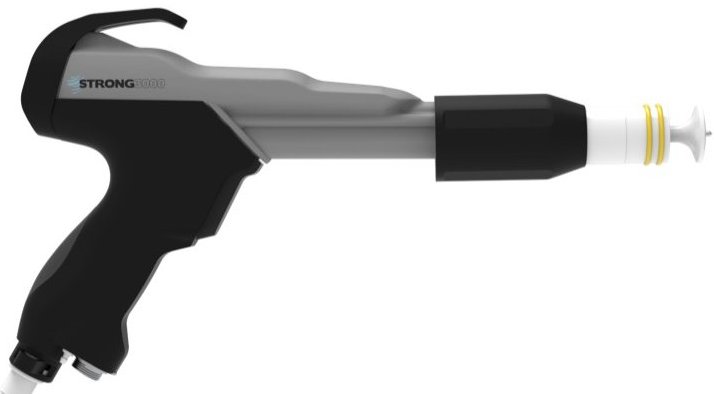
Powder Enamel Gun — Technical Specifications.
Values are typical ranges; final values are confirmed per project by STRONG3000 engineering.
| Application | Powder enamel (vitreous) |
|---|---|
| Output voltage | 0 – 100 kV (adjustable) |
| Wear set | Enamel-grade nozzle & electrode |
| Head groups | Part-specific head group options |
| Manual / Automatic | Both variants available |
From Powder to Finished Part.
Enamel Powder Feed
Enamel powder fed by abrasion-resistant injectors.
Electrostatic Charging
0–100 kV charging with enamel-grade electrode set.
Head Group Application
Homogeneous coating with part-specific head groups.
Recovery & Sieving
Overspray enamel is sieved and returned to the system.
Choose Your Setup.
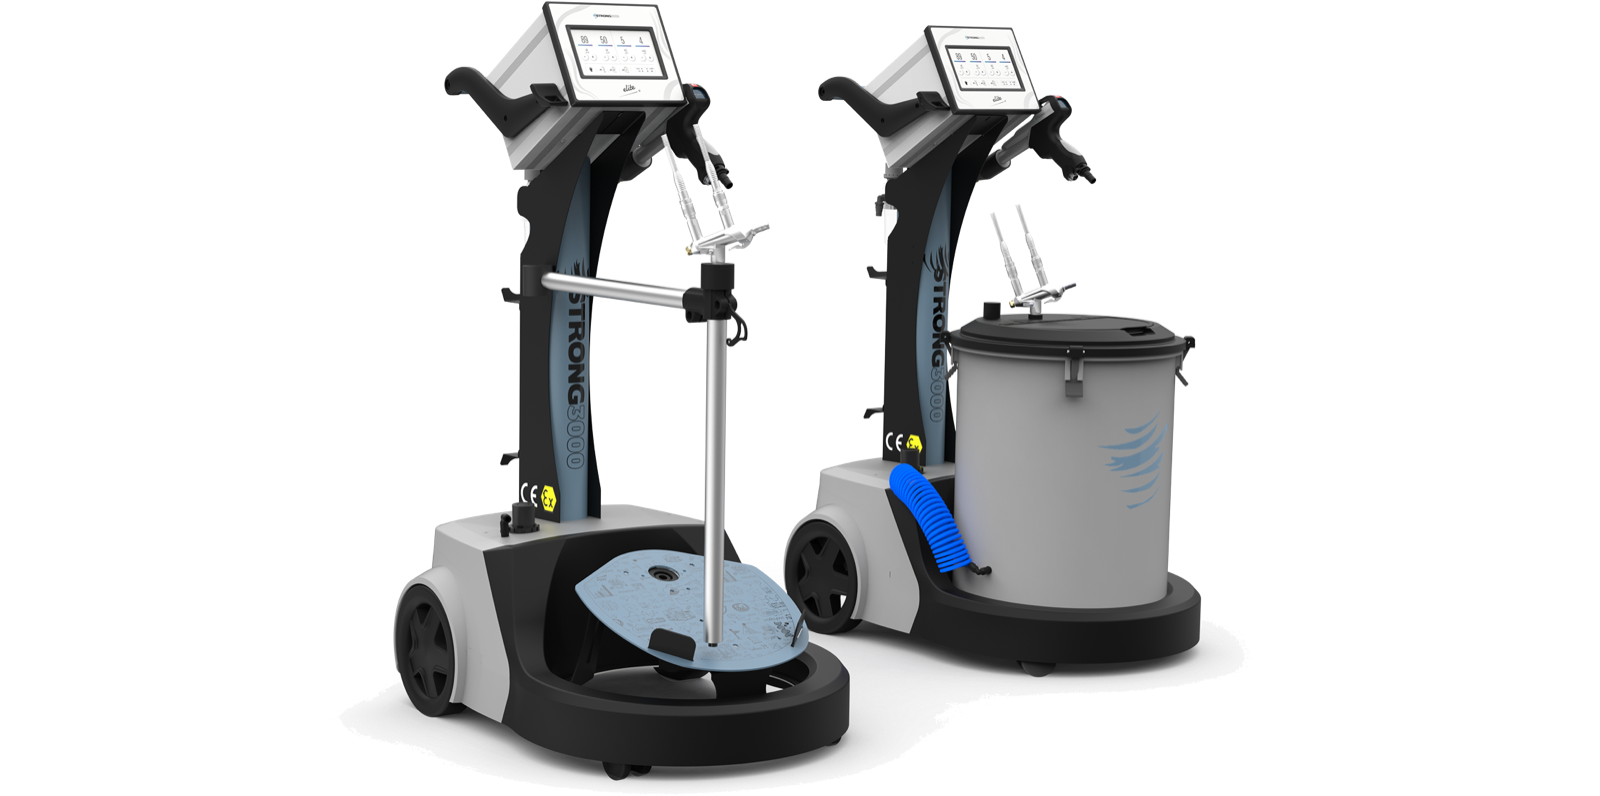
Manual Enamel Gun
Manual set for touch-up and low volume.
Automatic Short / Medium
Fixed mounting in line-type booths.
Head Group Options
Dedicated heads for cavity, burner cap, flat part and pipe.
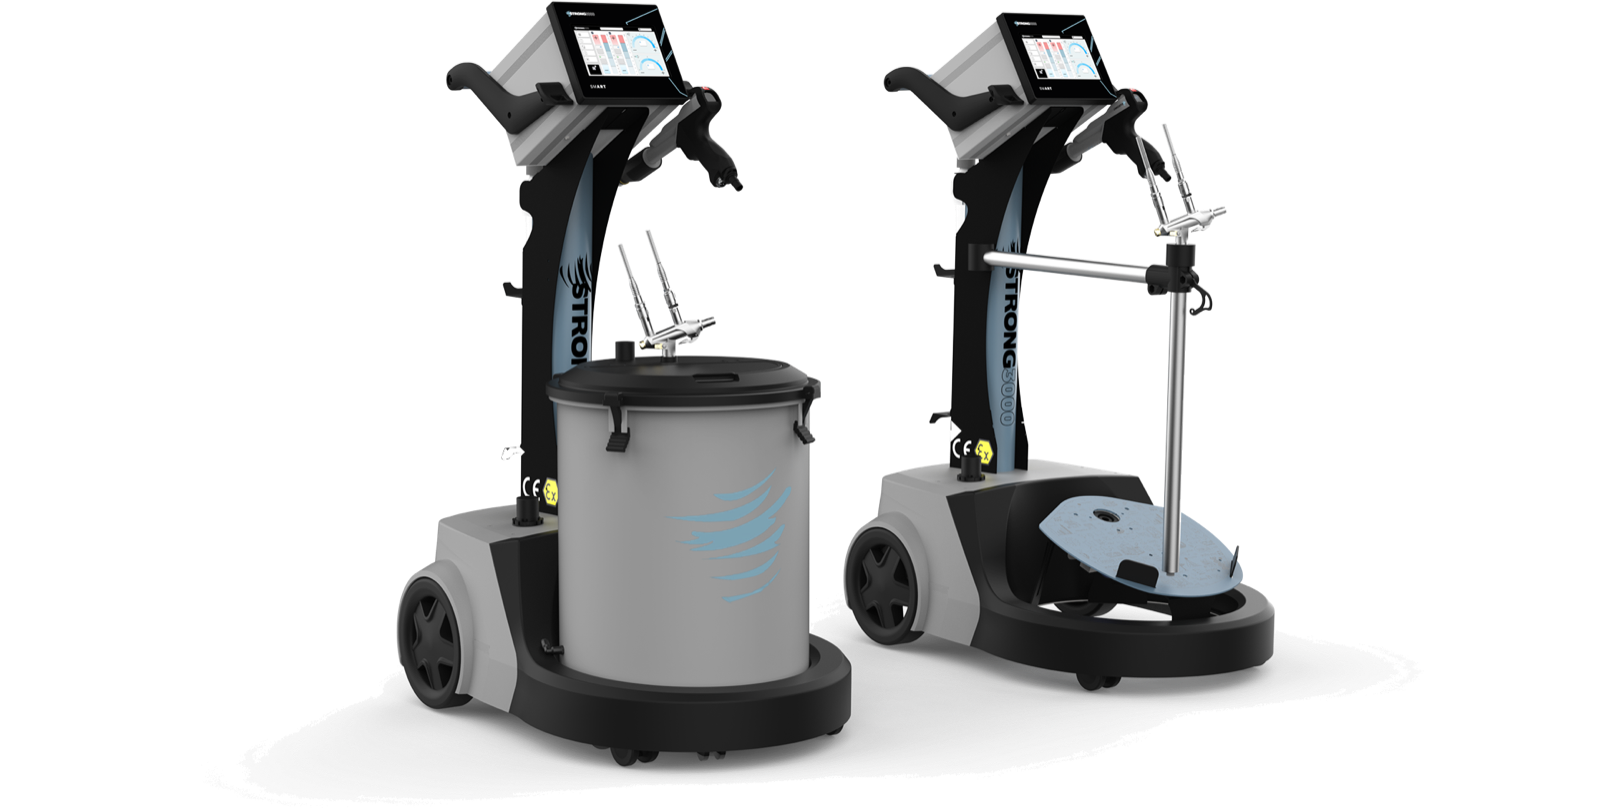
Part of the STRONG3000 System.
- Powder Enamel Booths — cavity / burner cap / pipe / stove
- Enamel Injectors — wear-resistant feed
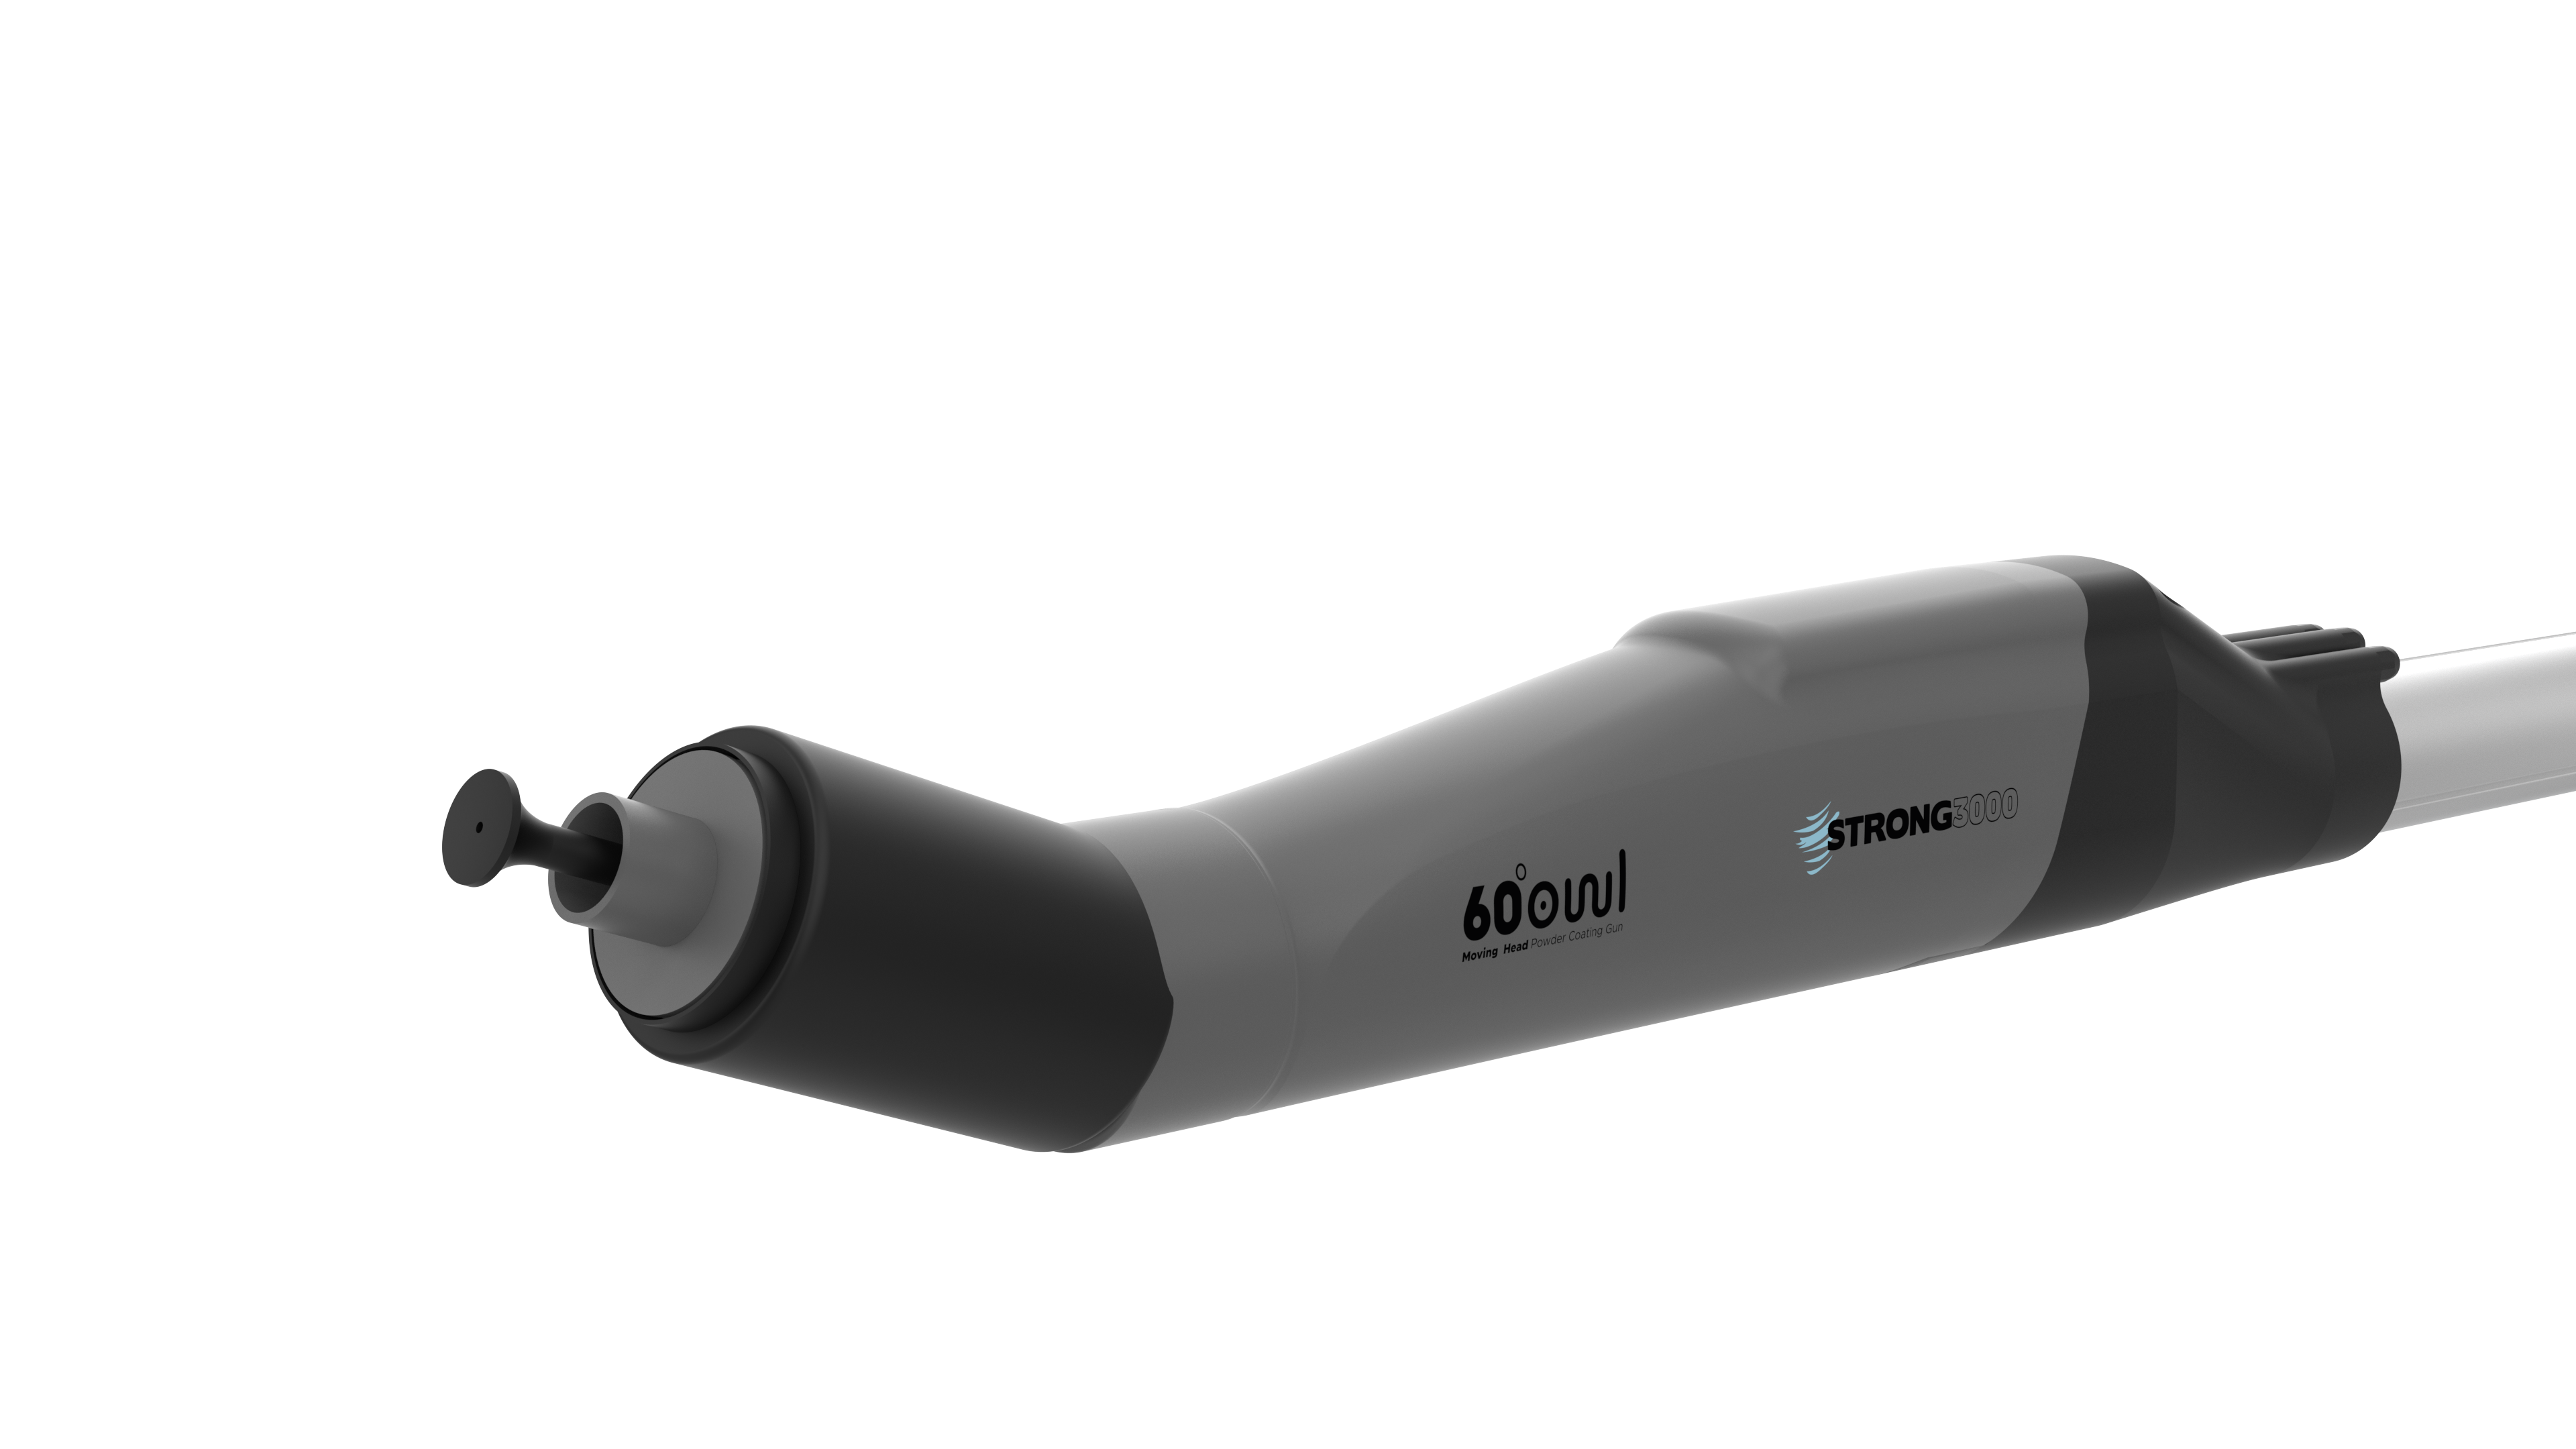
- OWL Intelligent Motion — access to deep geometry
- Ultrasonic Sieving — enamel-grade recovery
- Enamel Firing Ovens — 780–860 °C line integration
Technical Datasheet & Documents.
PDF · All the technical content of this page
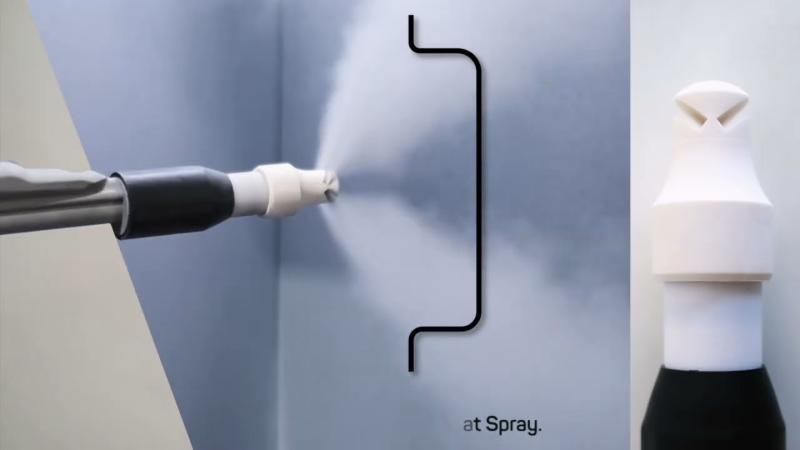
See It in Action.
 0:33
Complete the System.
Frequently Asked Questions.
Enamel powder is glassy and abrasive; nozzles, electrodes and powder paths are made of abrasion-resistant materials.
Yes. OWL's head motion is particularly effective in cavity enamelling.
It depends on usage intensity; the set is quick-change and supplied from stock.
Real Lines. Real Work.
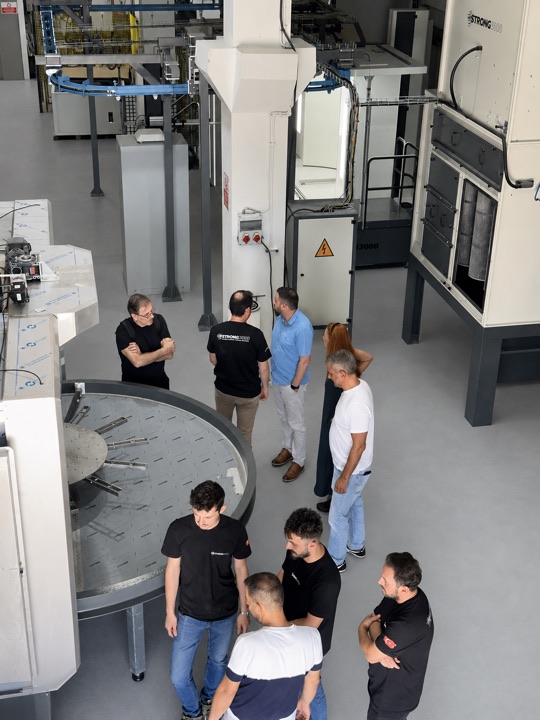
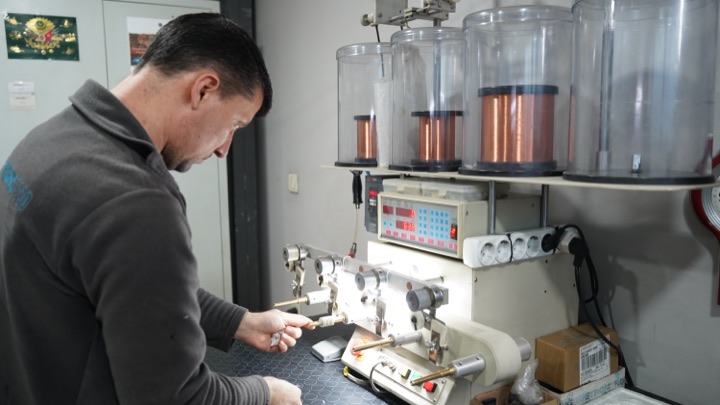
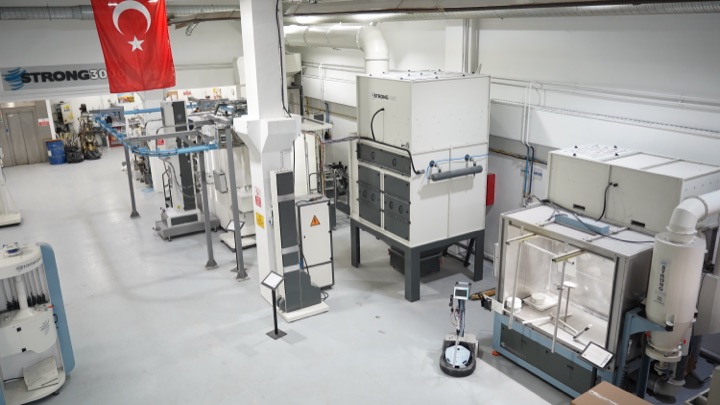
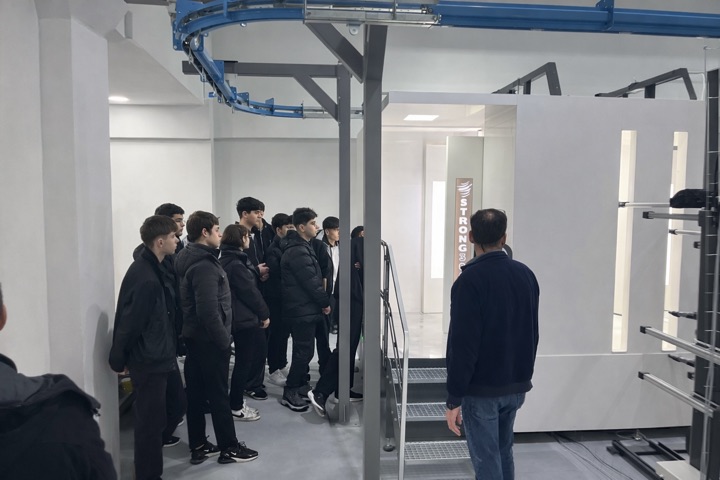
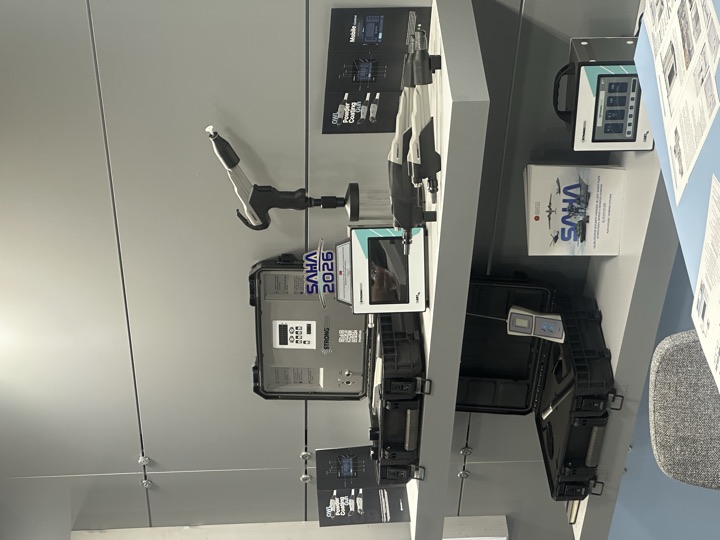
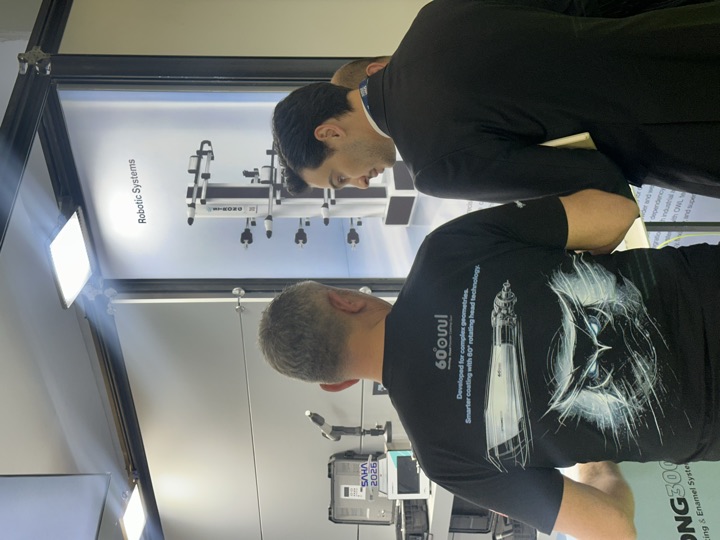
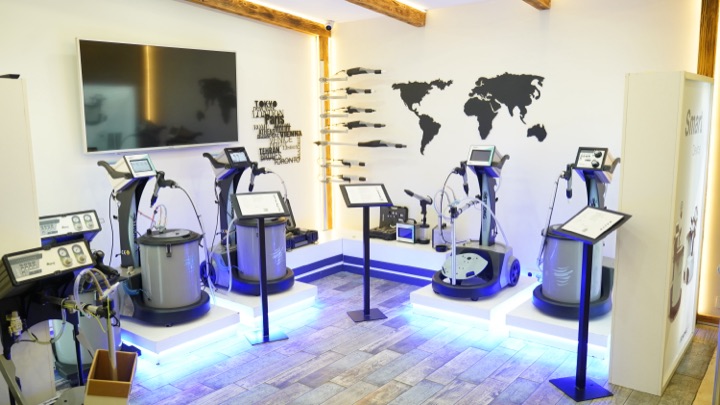
See our equipment running in our showroom and on our production line. Book a visit — our team will host you at our facility for a live demo, sample application and line planning.
Applying Powder Enamel?
Tell us about your part and frit type — we'll recommend the right powder enamel gun configuration.