EN/TR

EN / TR

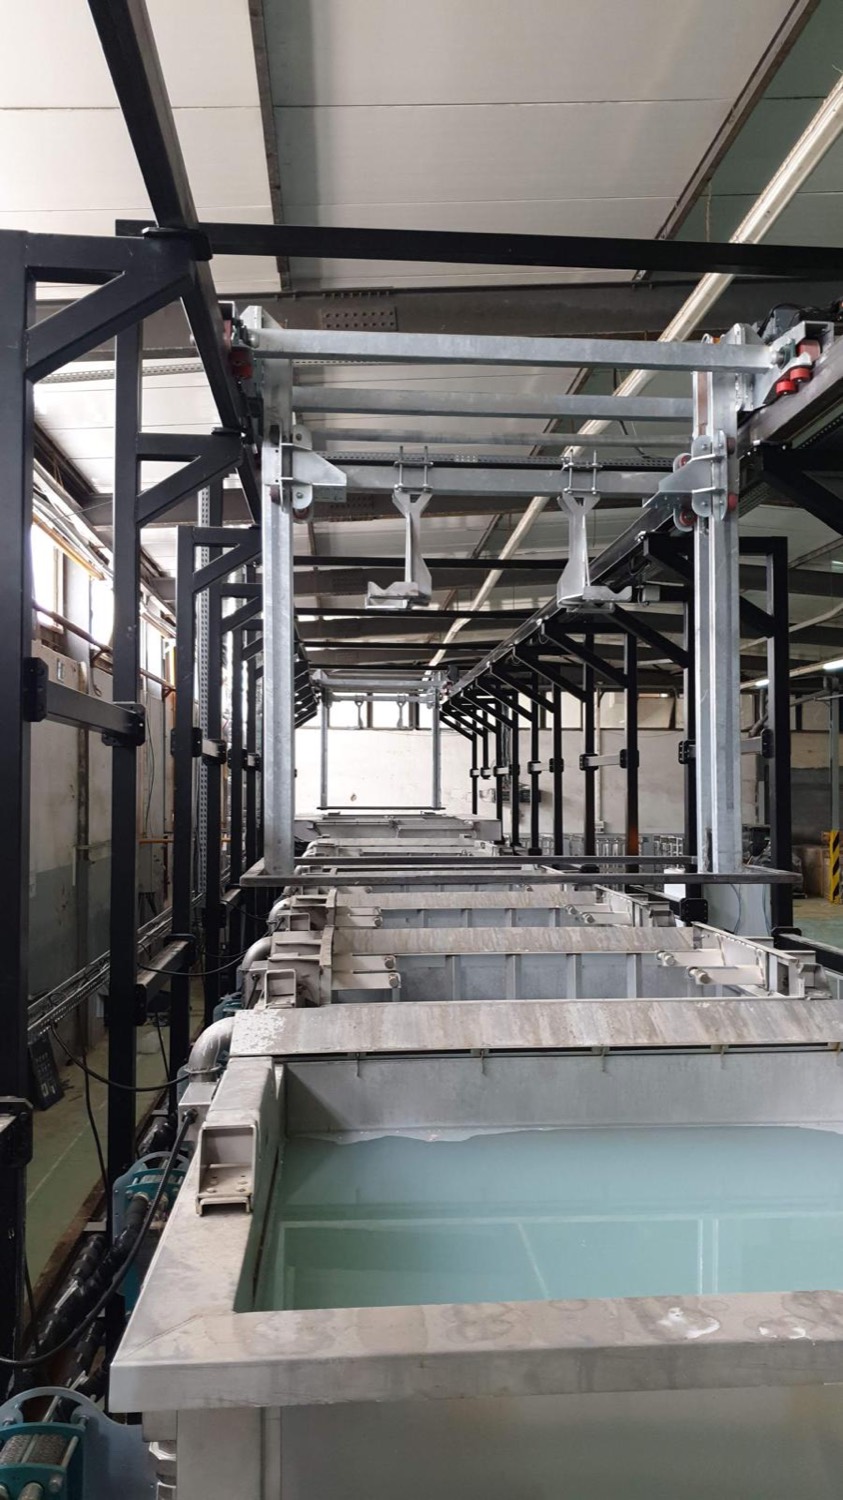
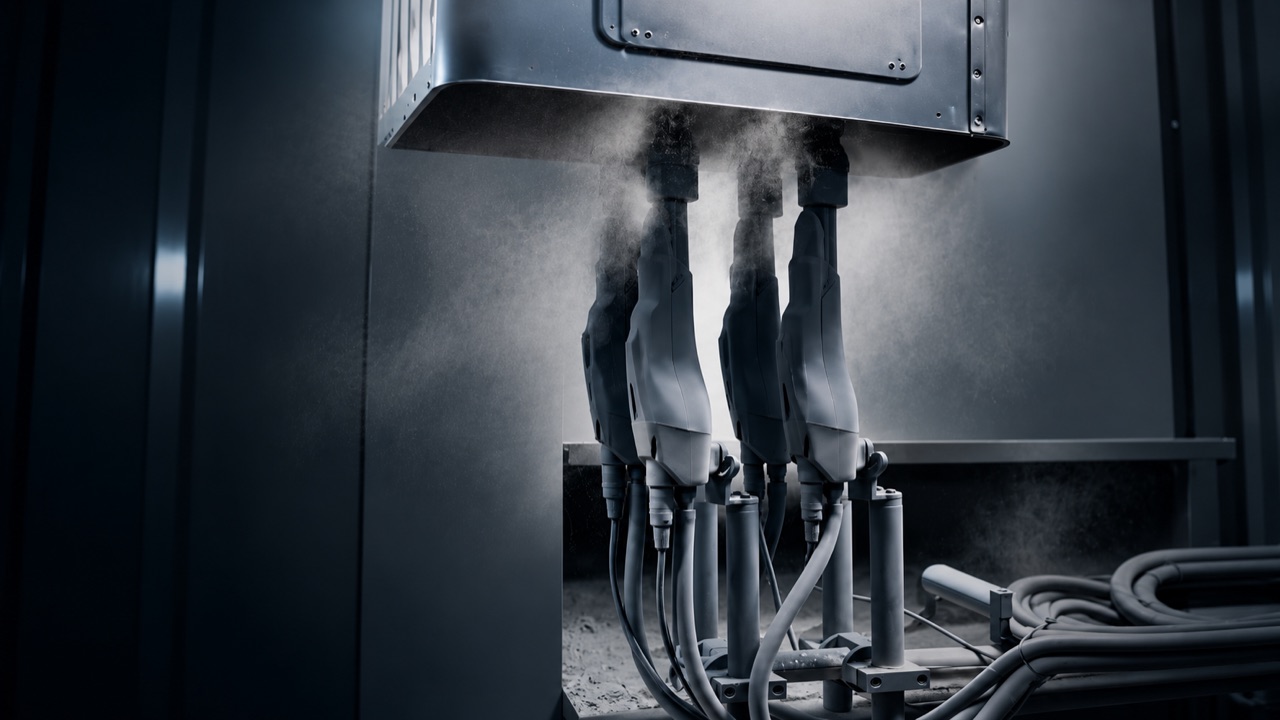
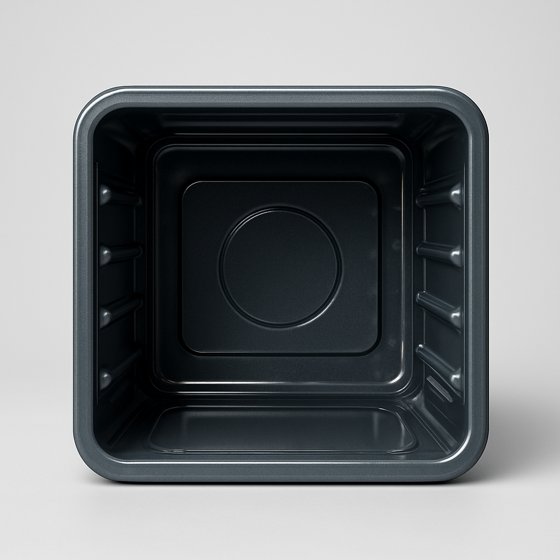
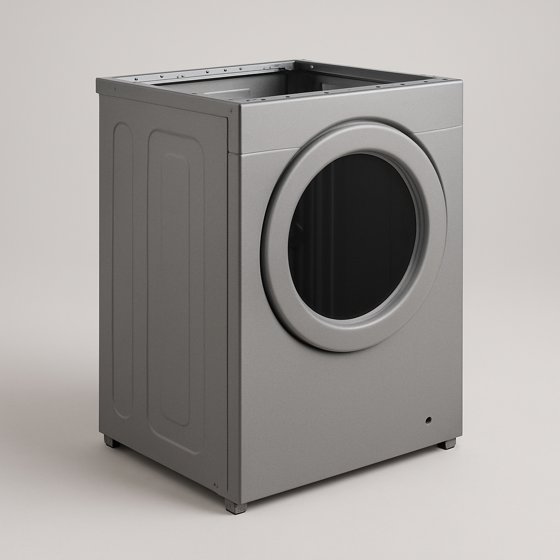
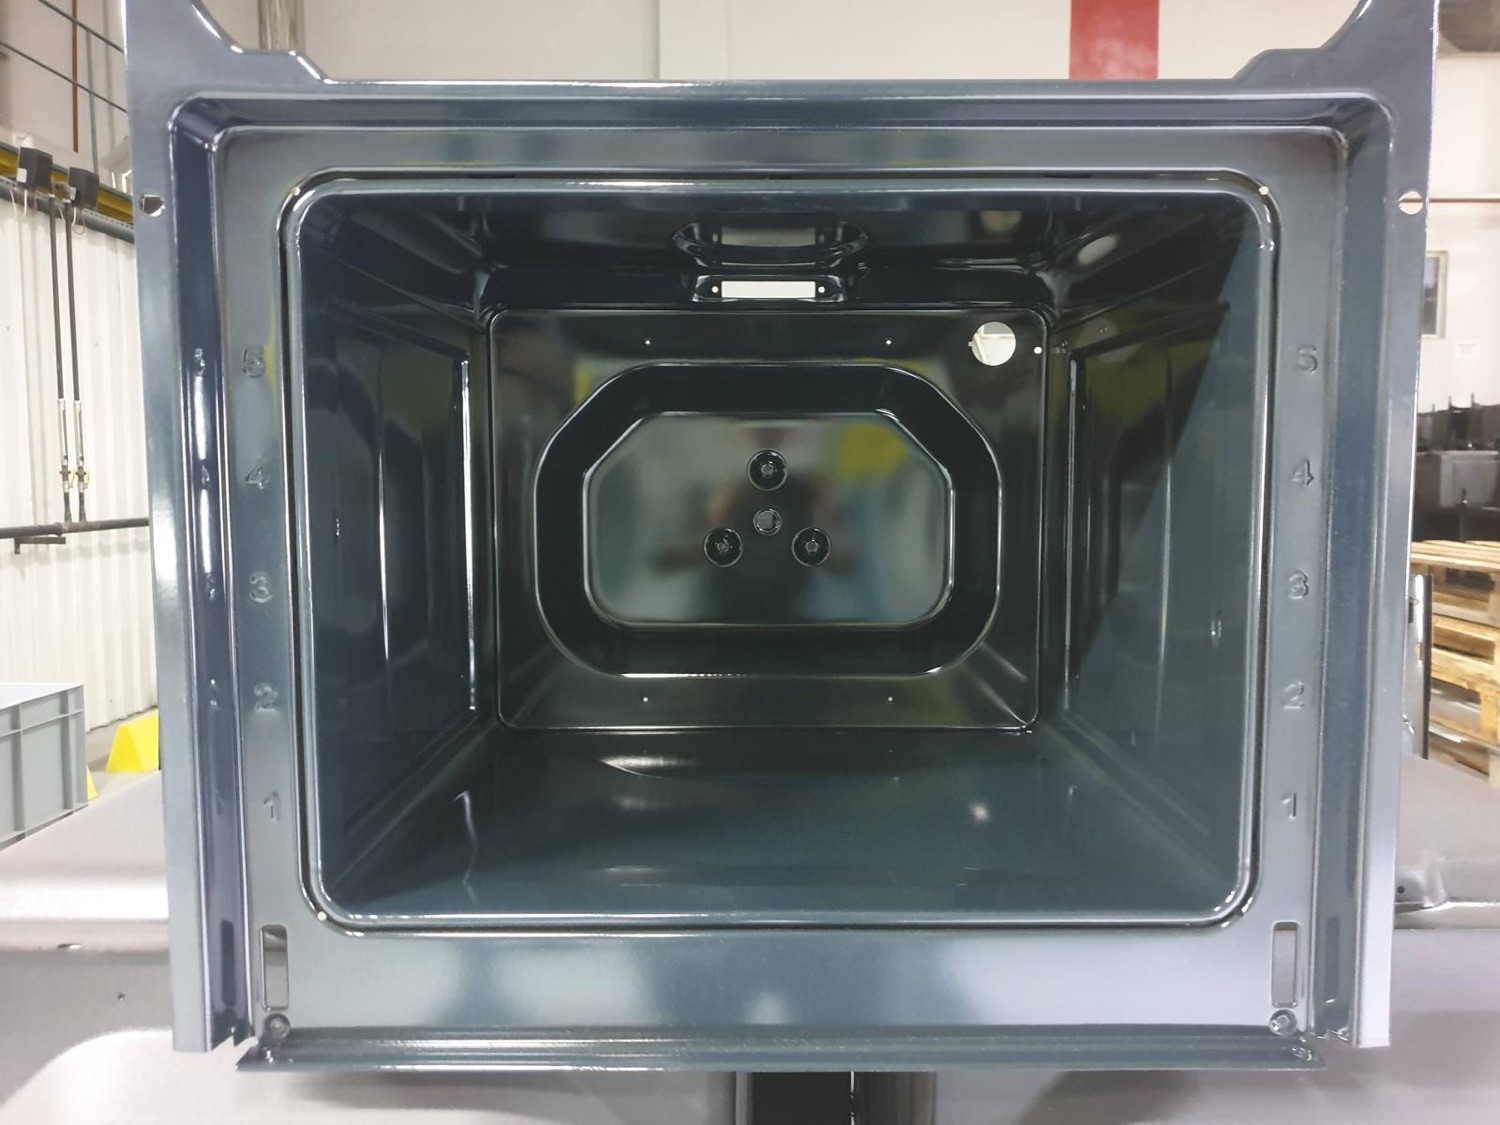
Powder-enamelled oven cavity
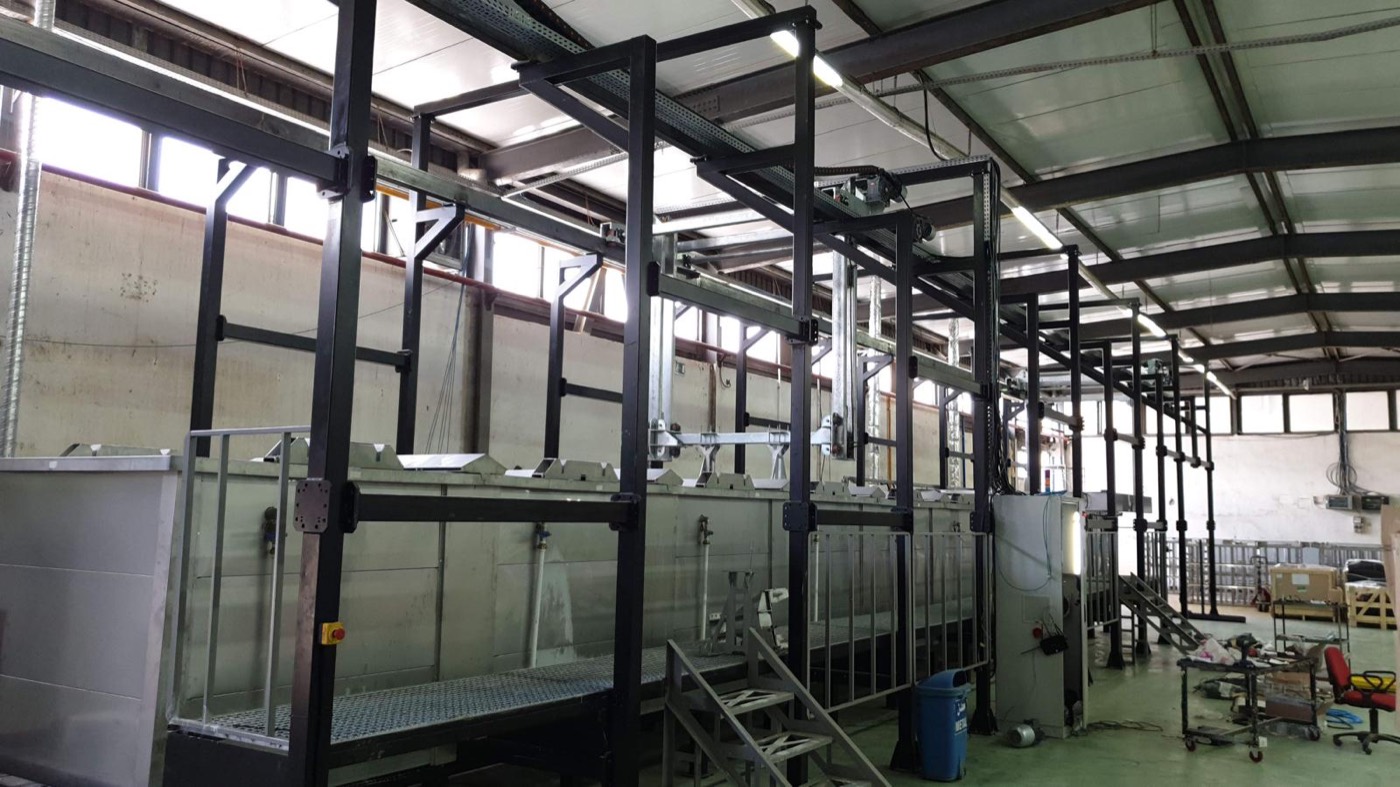
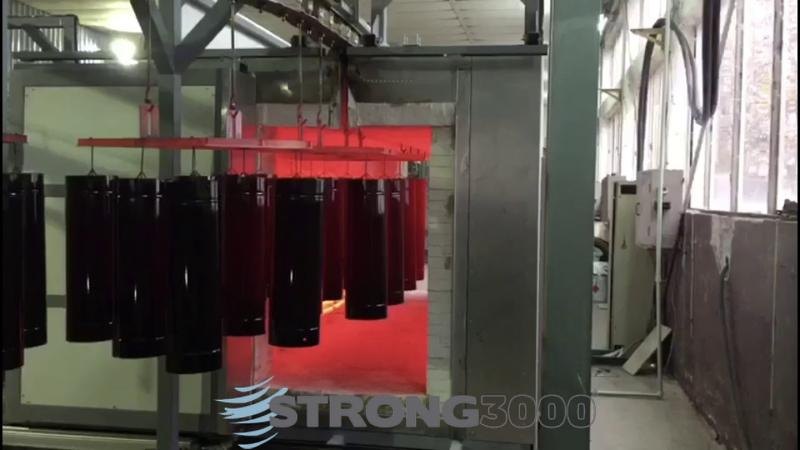
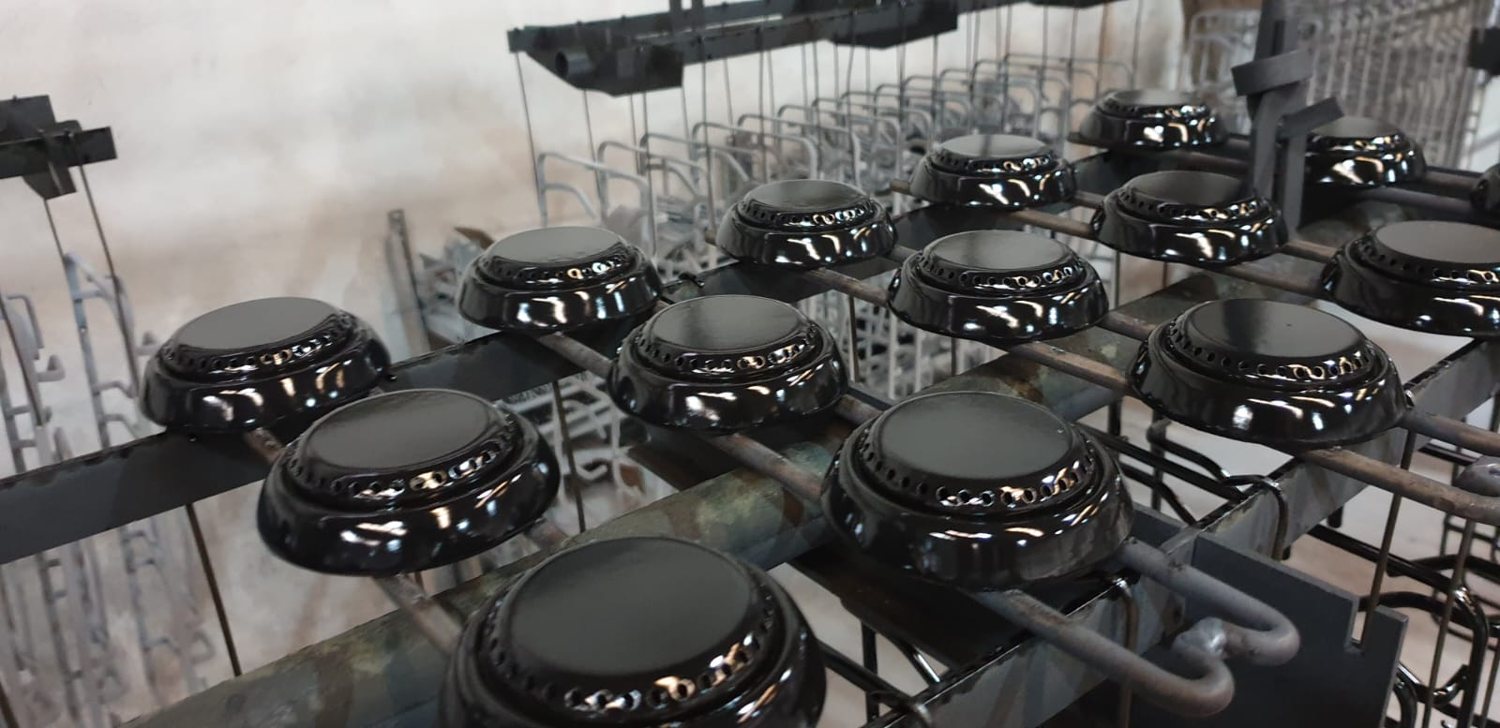
Burner cap enamel line
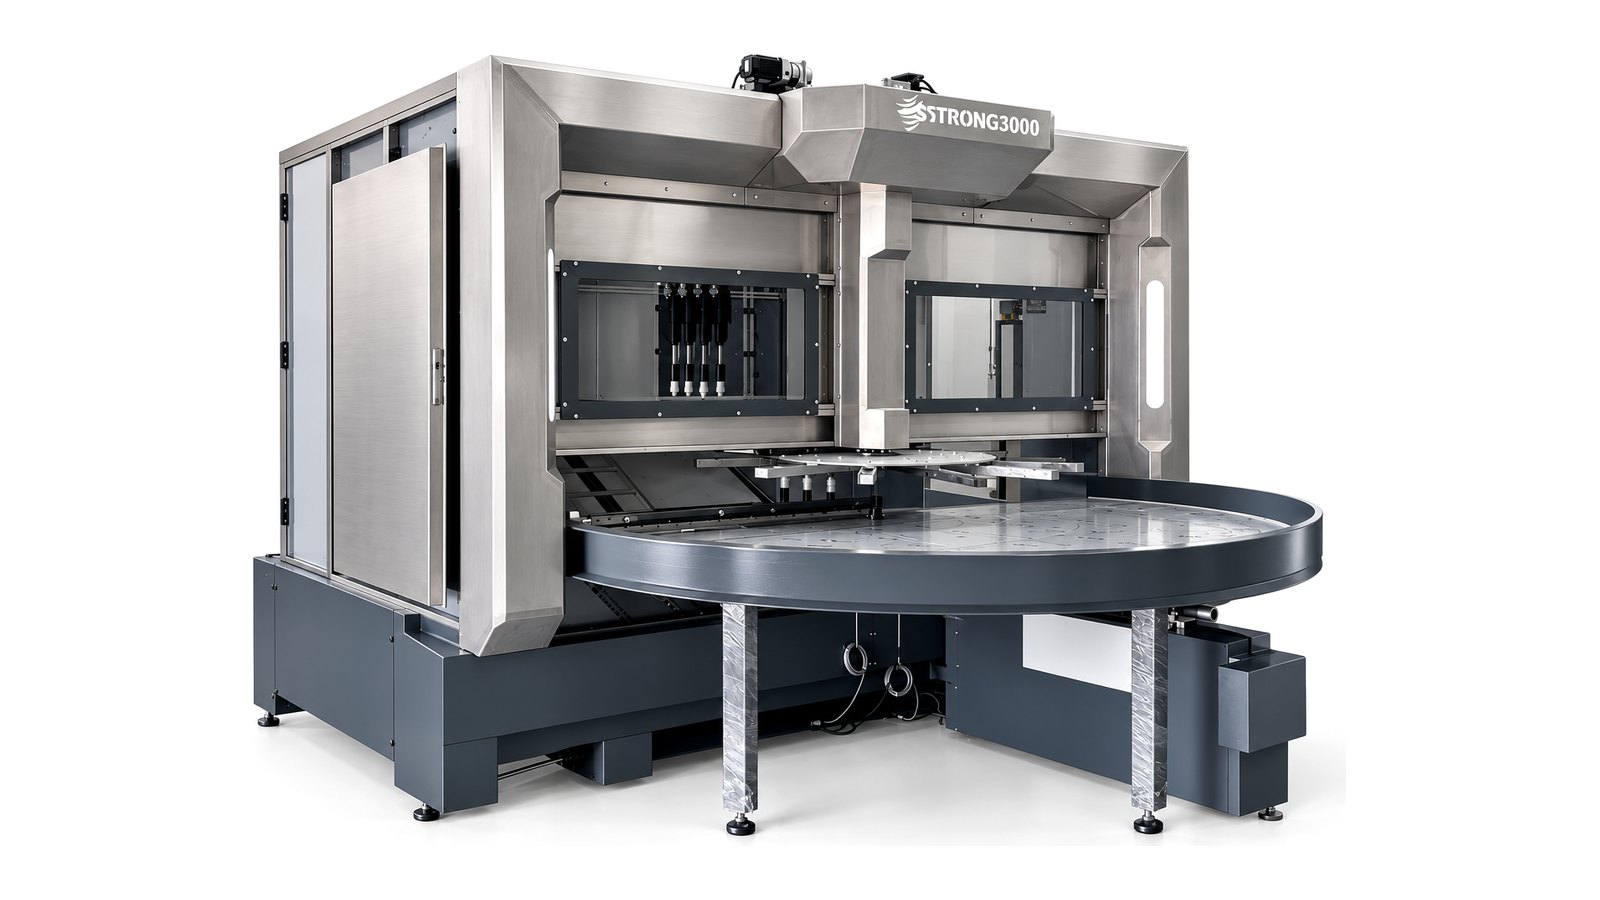
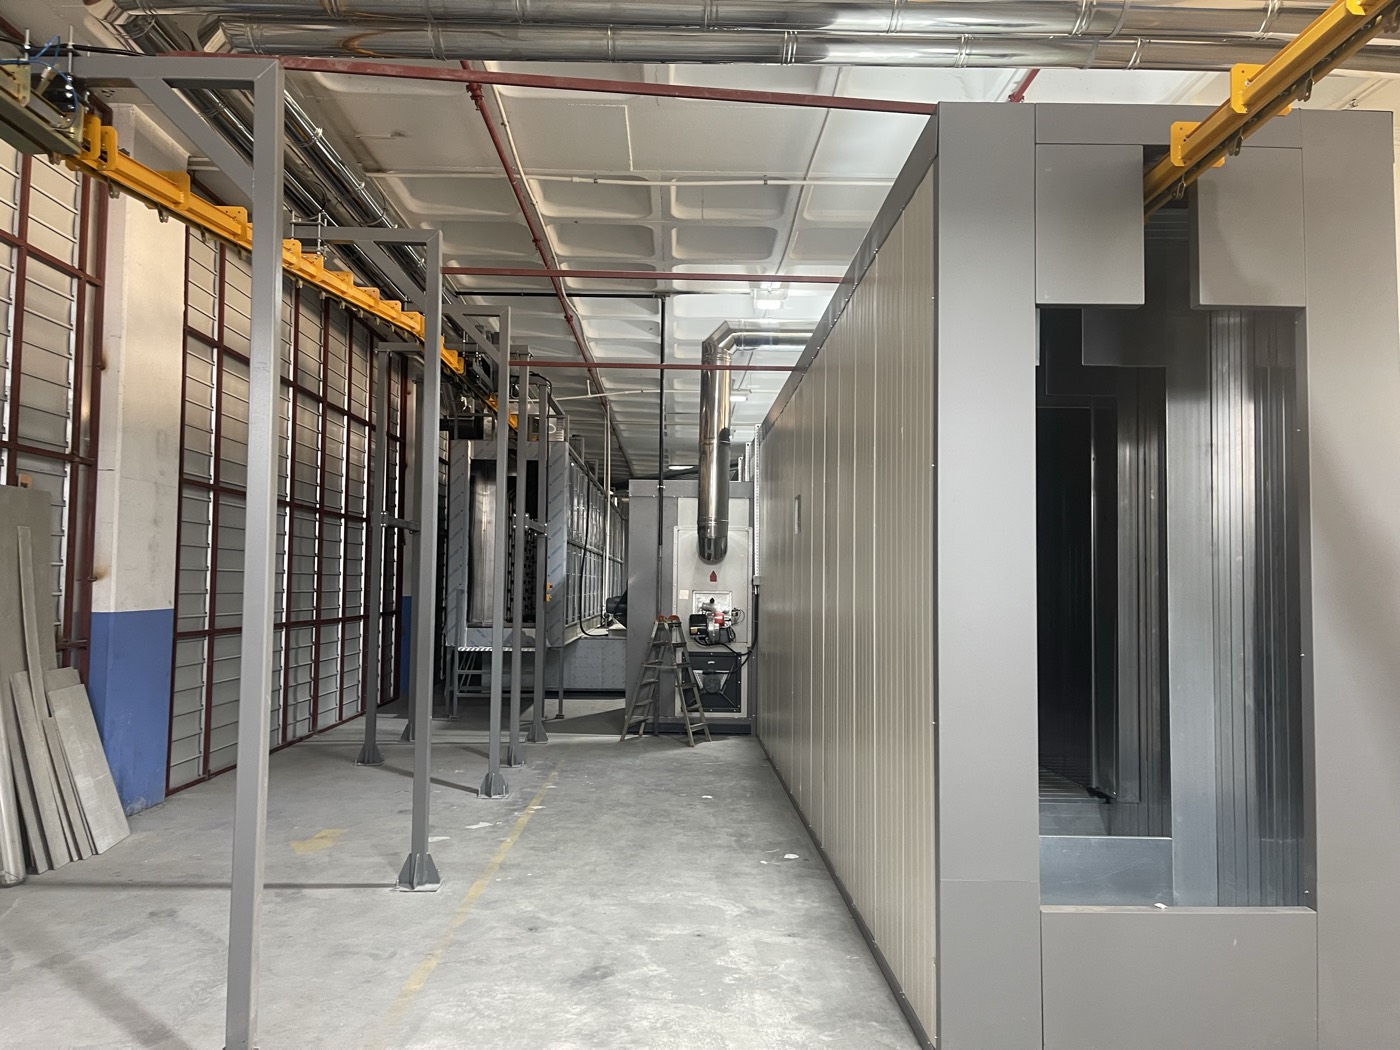
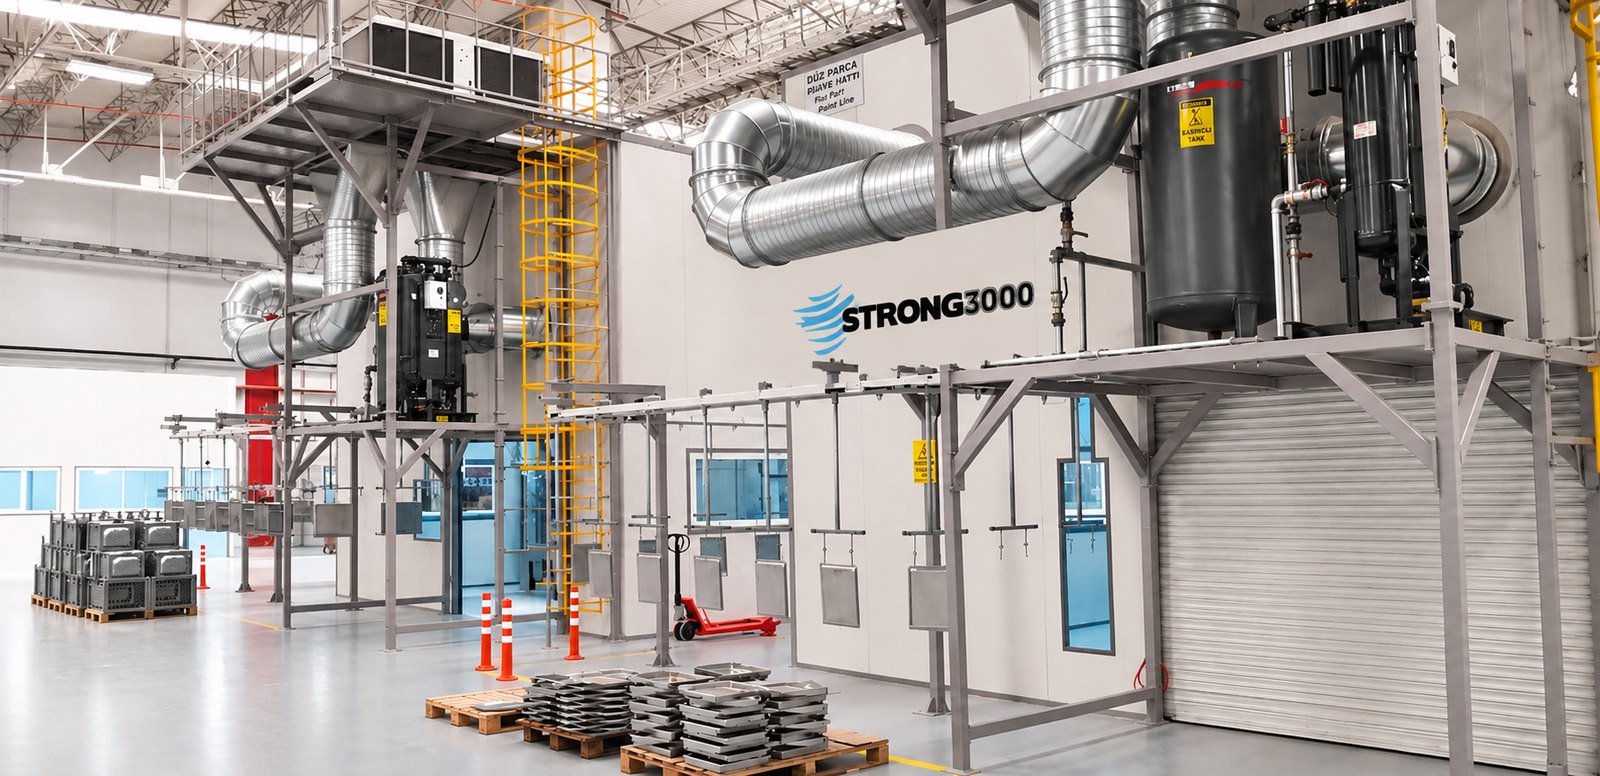
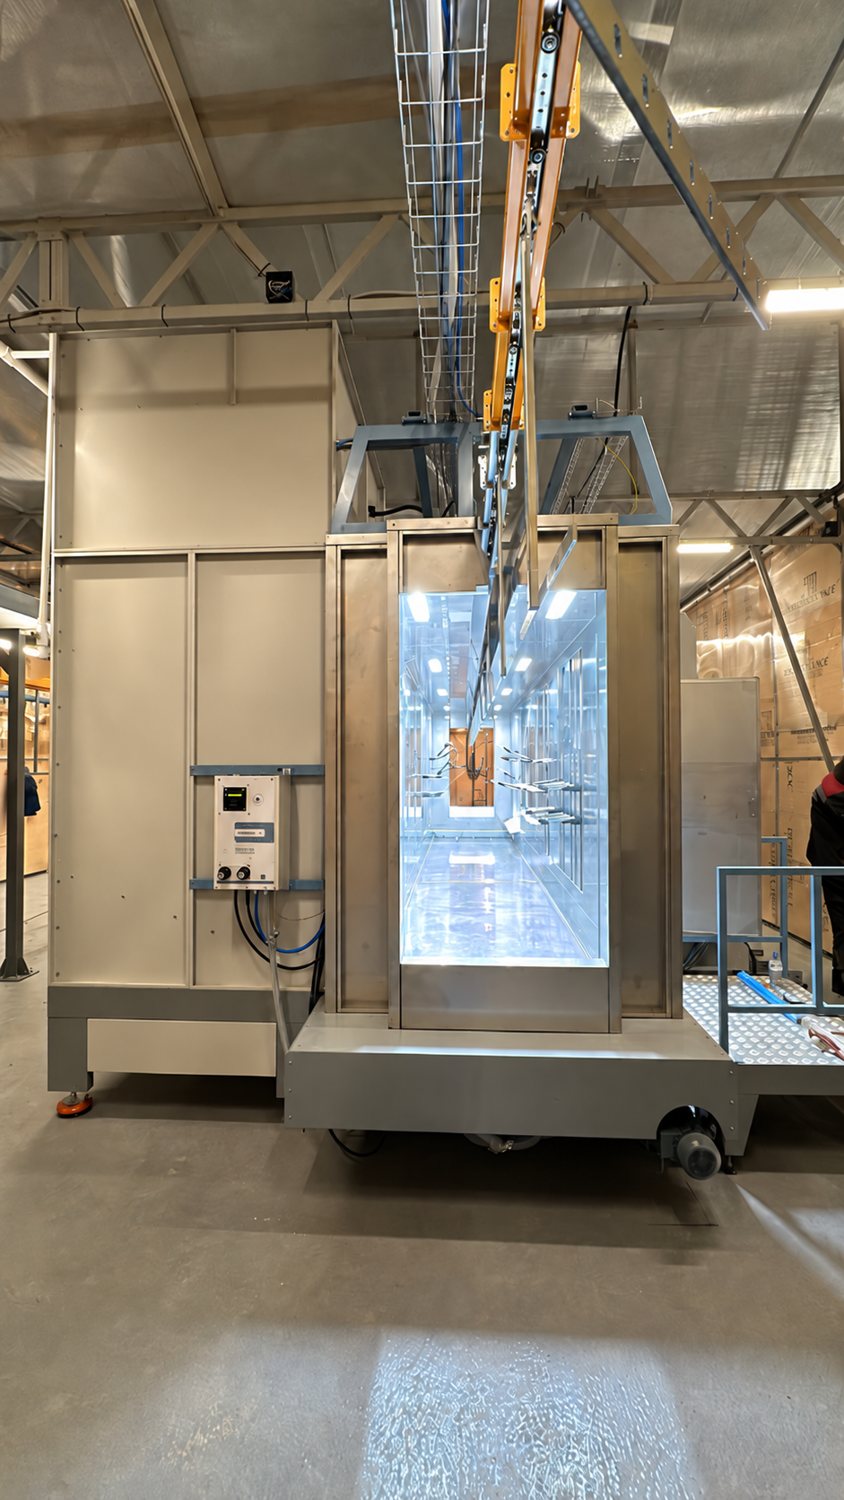
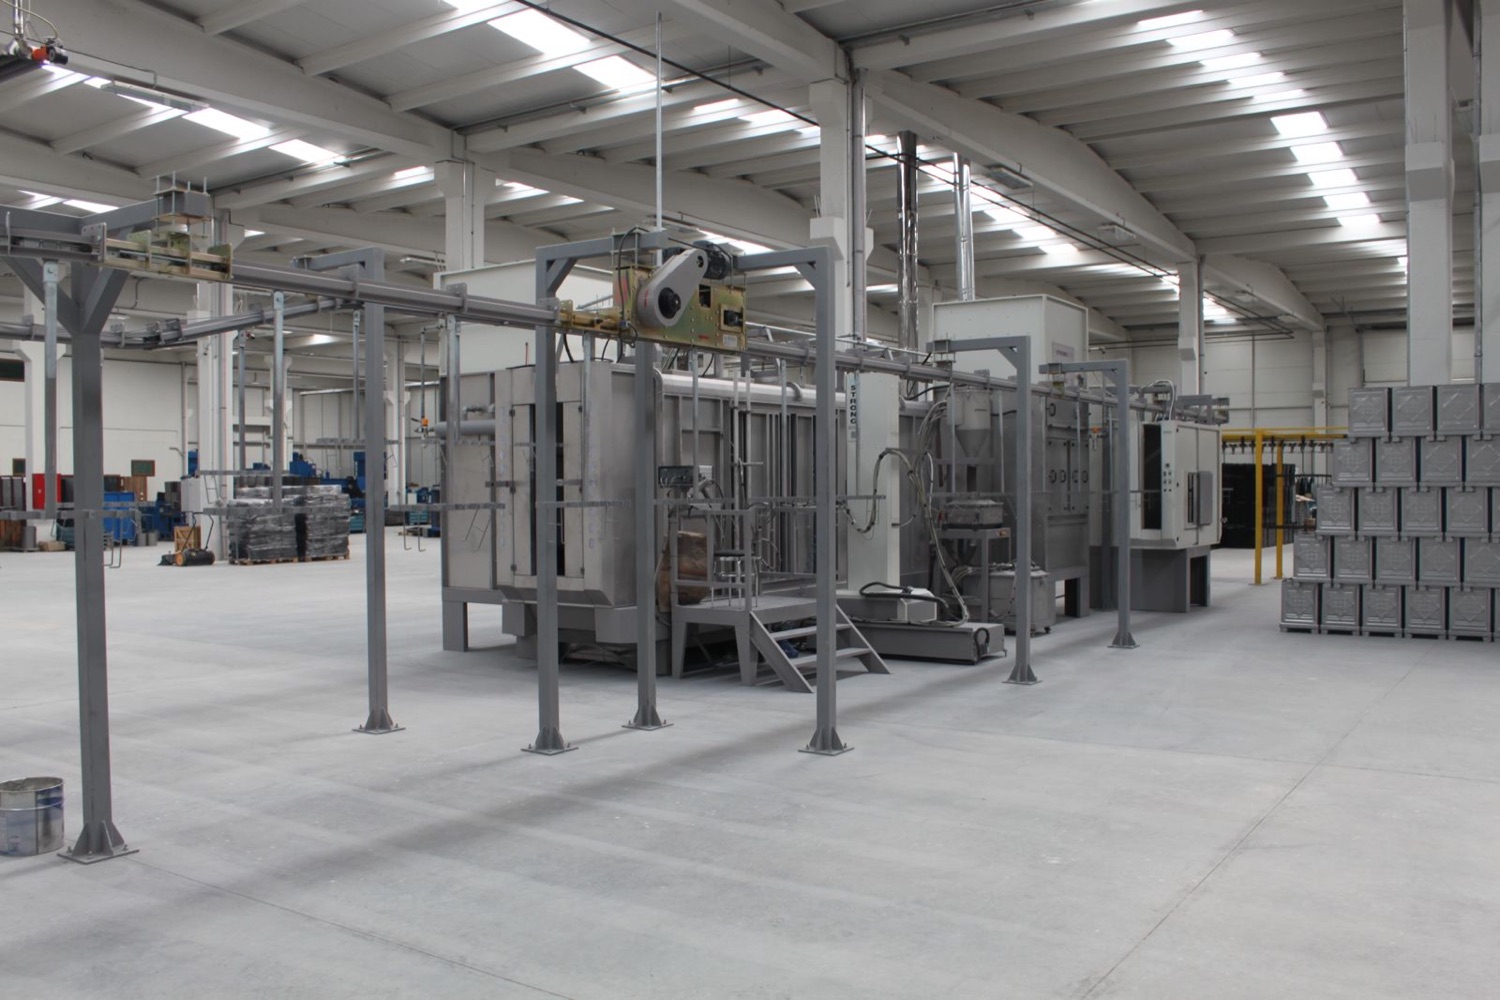
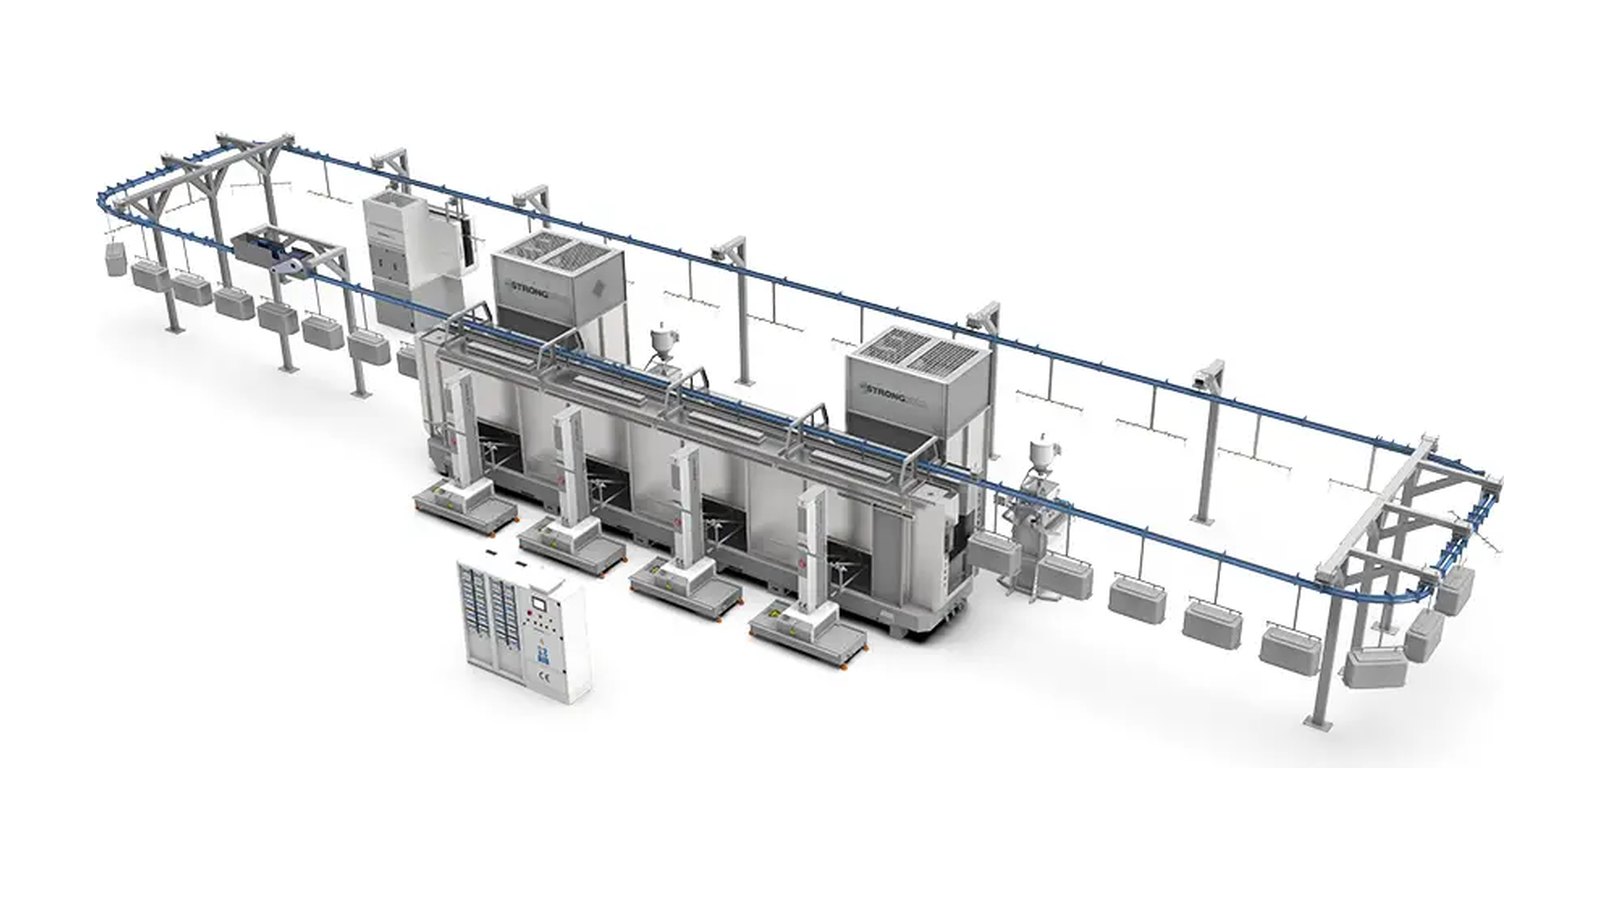
Flat part powder enamel plant
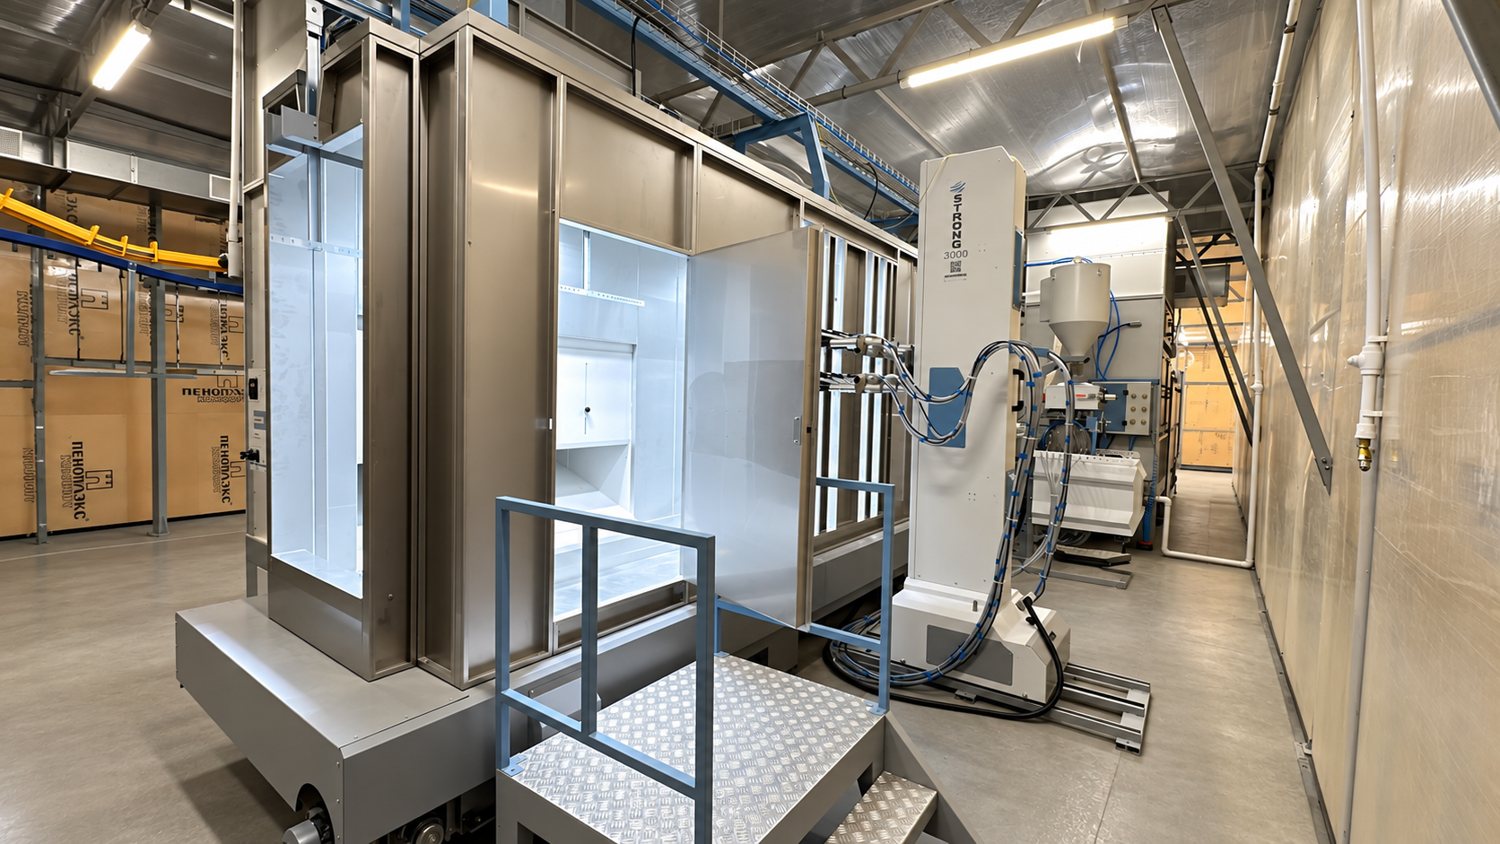
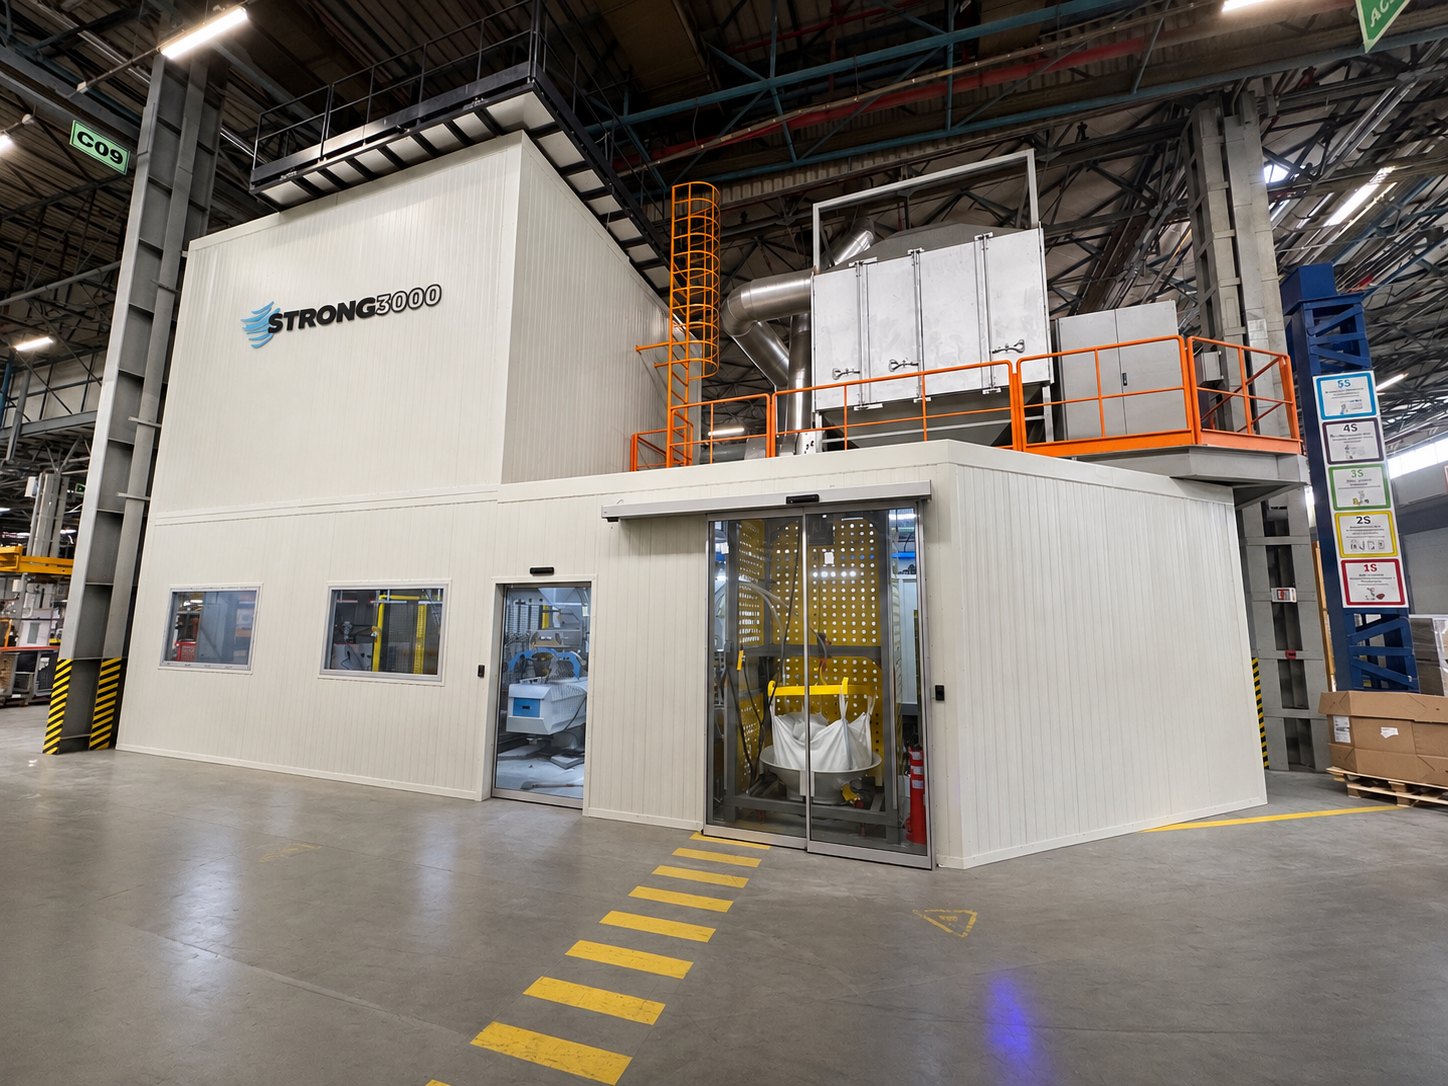
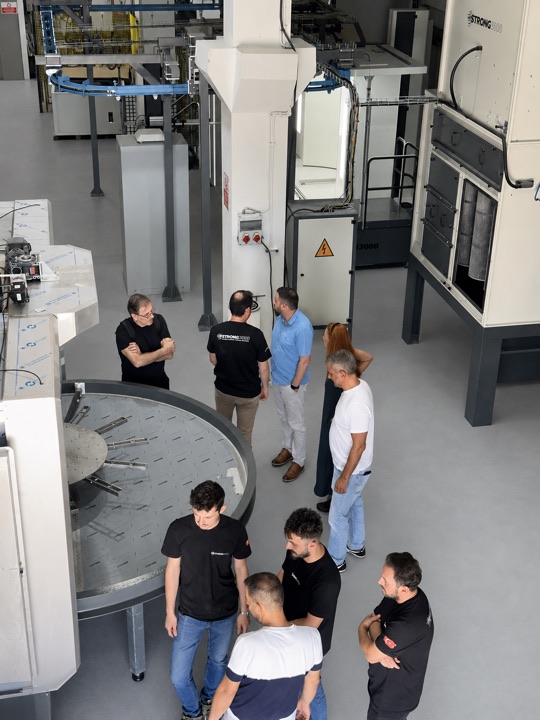
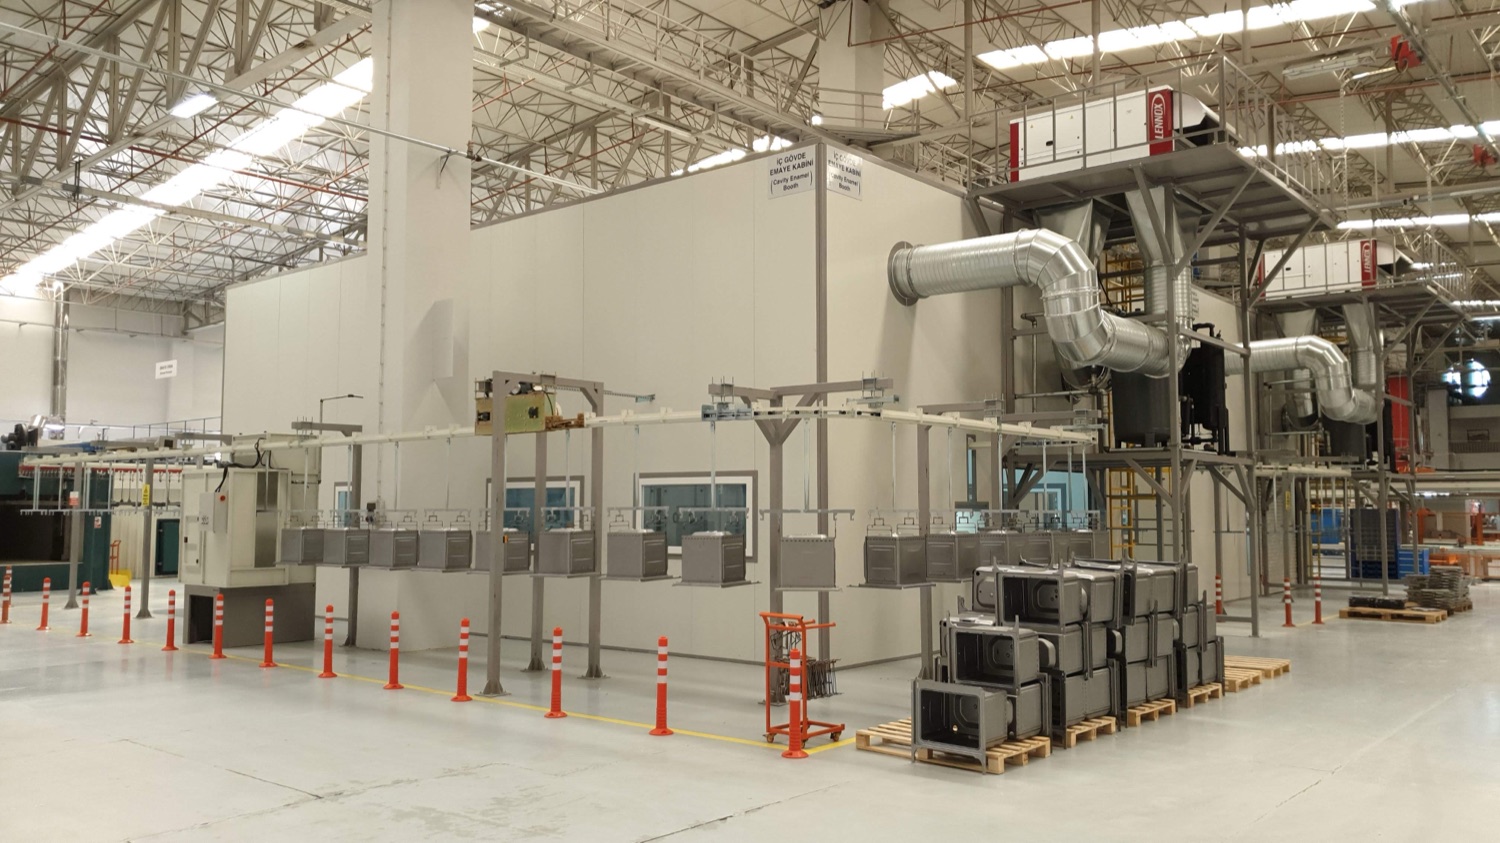
Cavity powder enamel plant
Solutions · Powder Enamel

Turnkey Powder Enameling Lines

Vitreous and porcelain enamel — a glass finish fused to steel and cast iron at high temperature. A core STRONG3000 engineering specialty, distinct from powder coating.

Enamel vs. Paint Download Technical Datasheet
System Overview

Glass Fused to Metal.

Powder enameling applies a vitreous (glass-based) enamel powder to metal parts, which is then fired at high temperature so it fuses into a hard, glass-like surface. The result is a finish that resists heat, corrosion, chemicals and abrasion far beyond an organic coating.

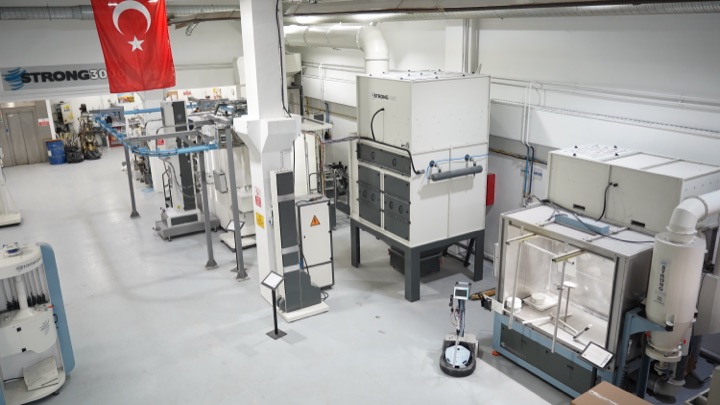
STRONG3000 engineers the complete enameling line — pretreatment, application, drying, high-temperature firing, powder recovery and automation — with deep experience in flat, deep and cavity part geometries.

Our Automatic Systems
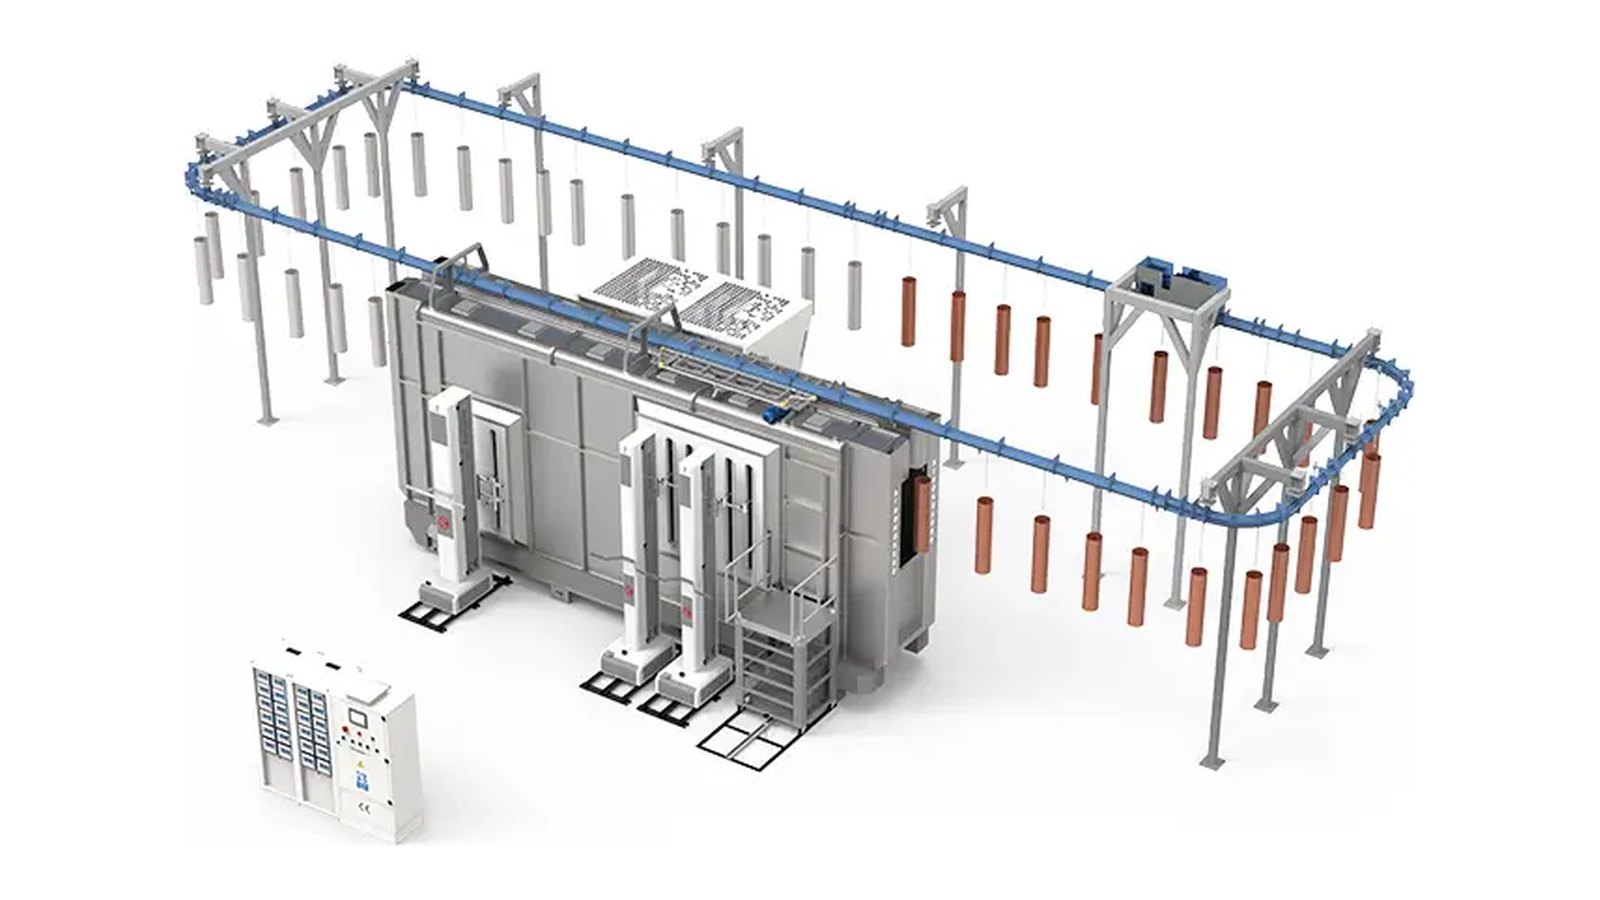
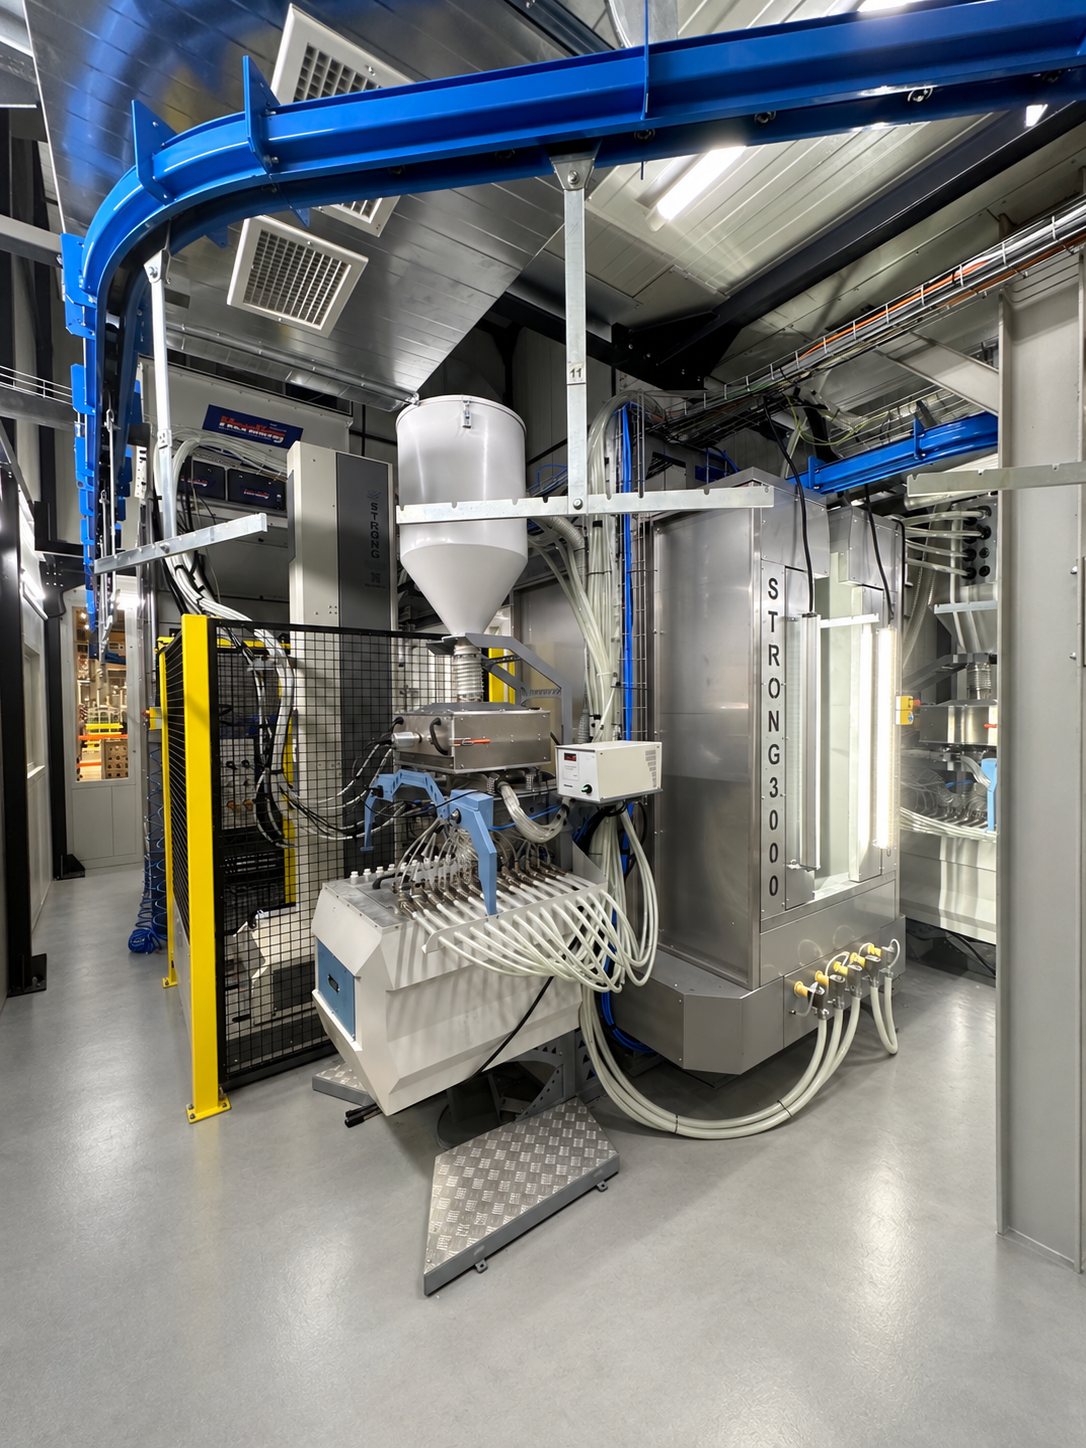
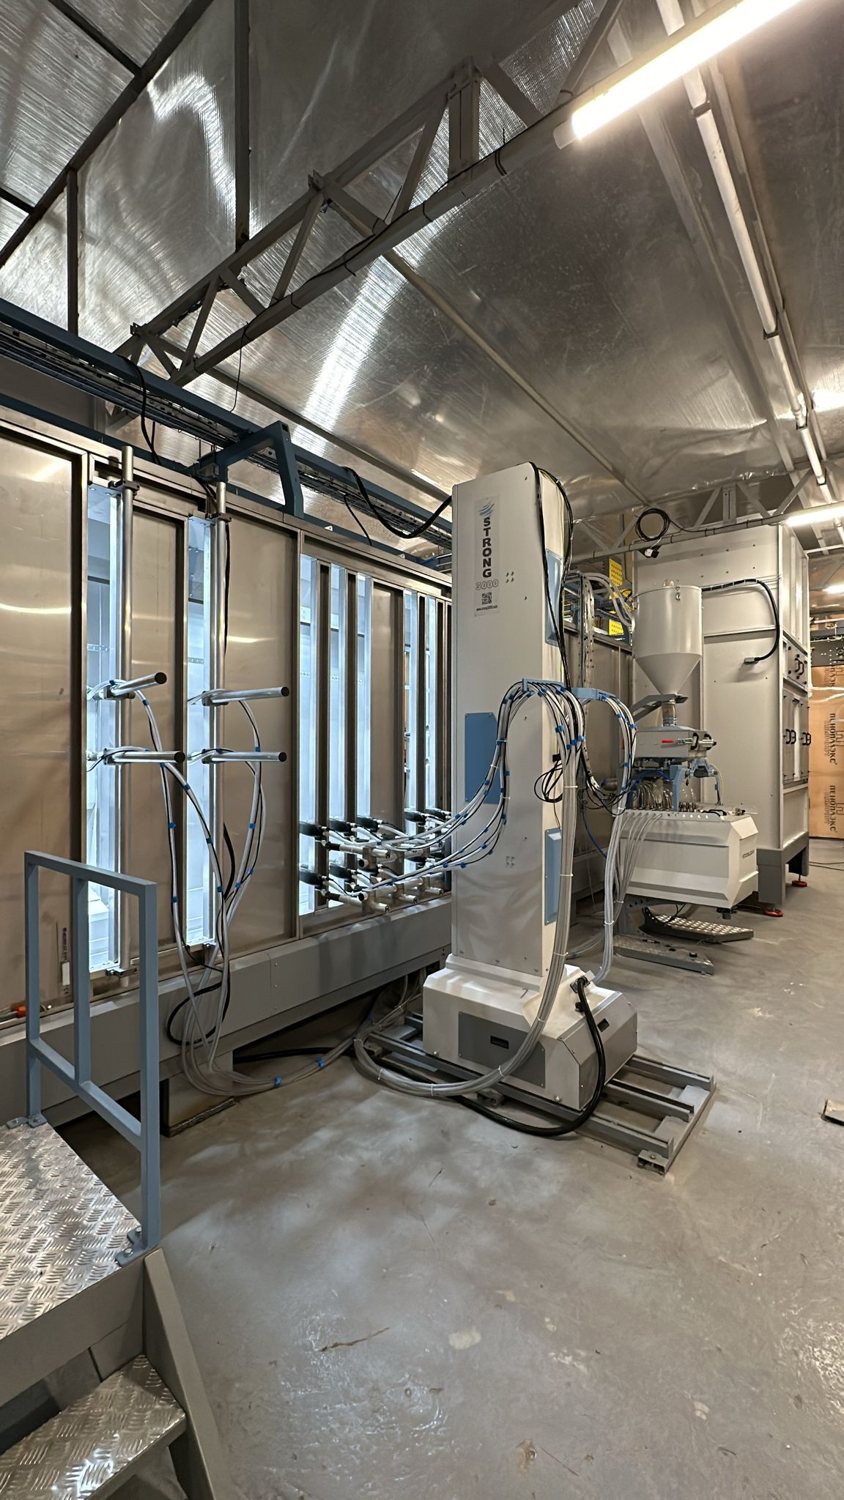
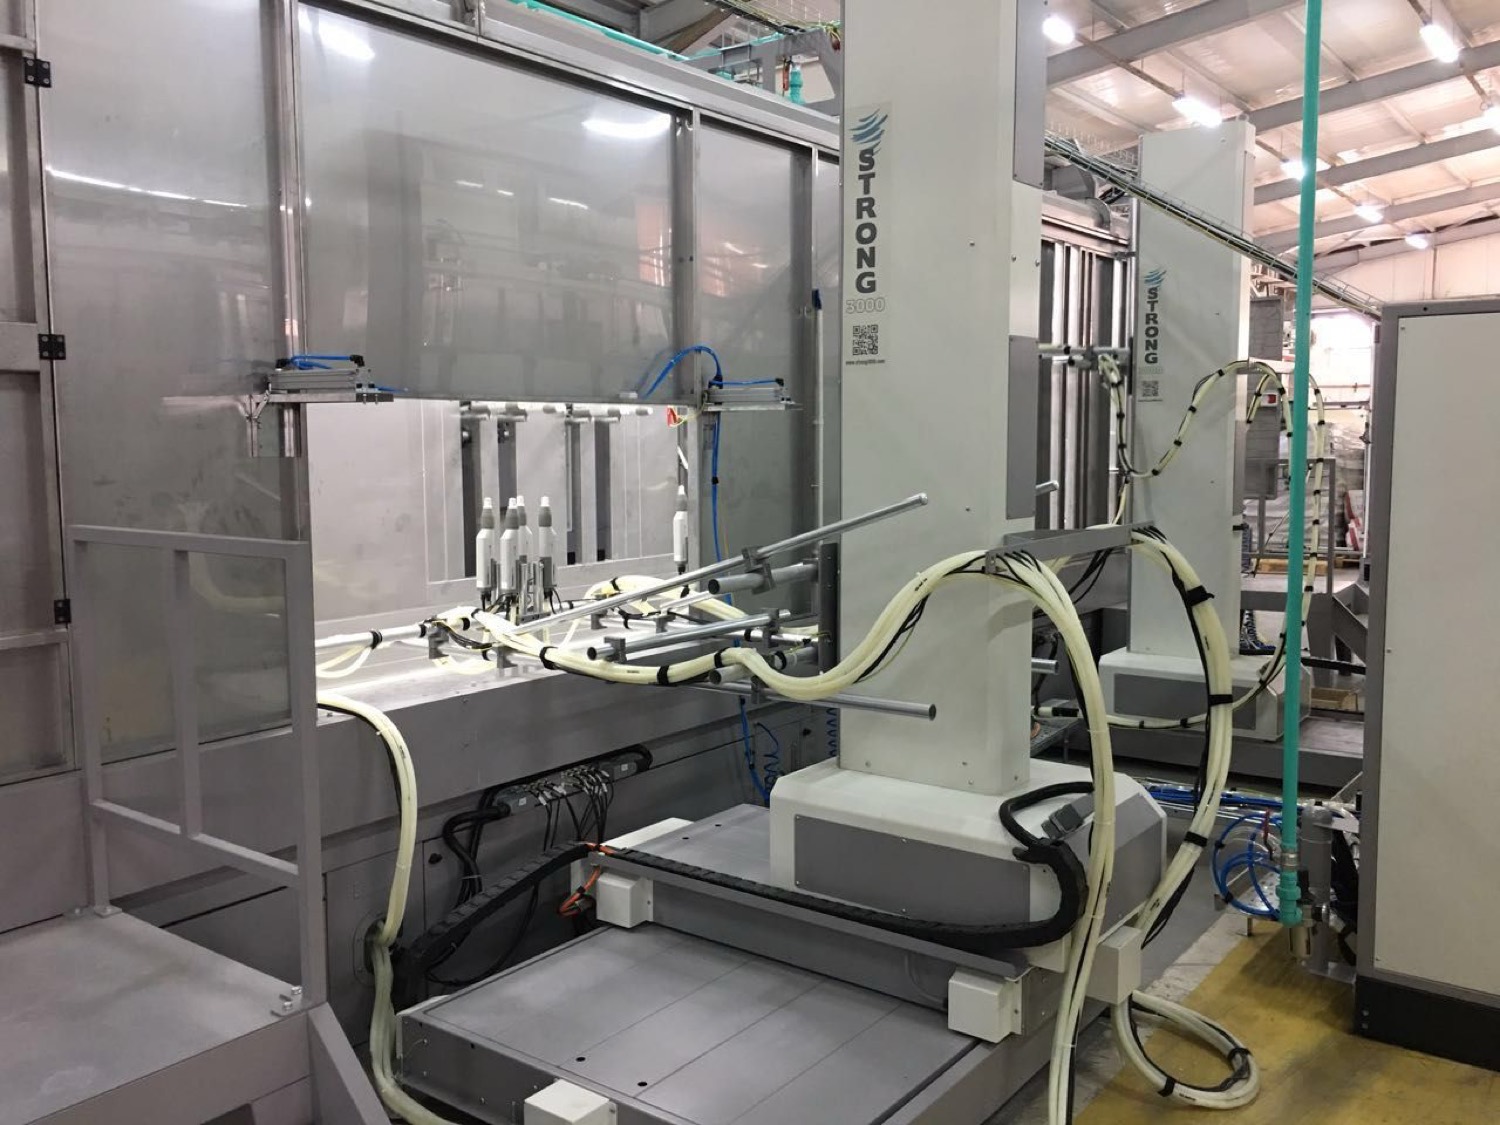
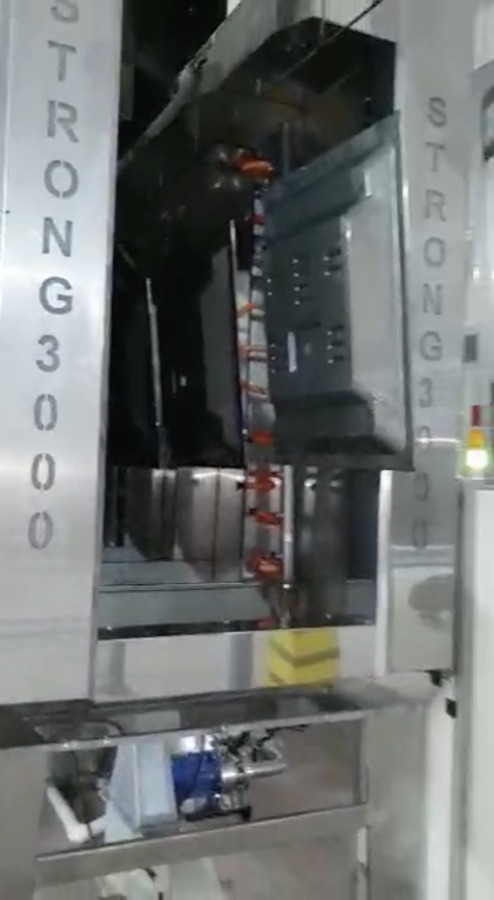
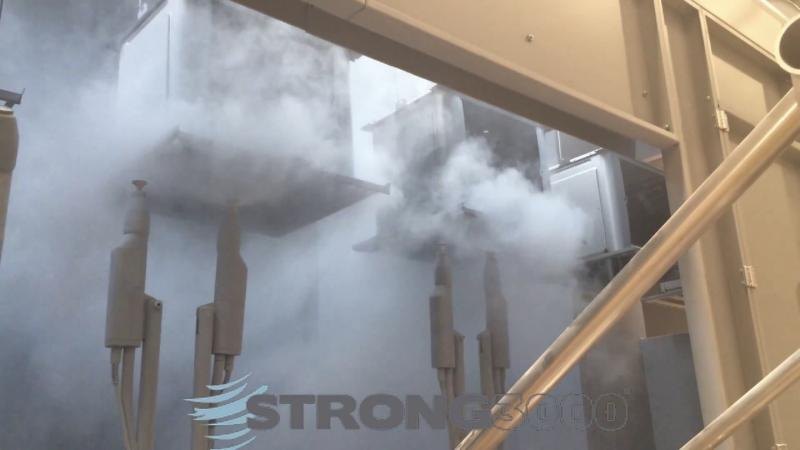
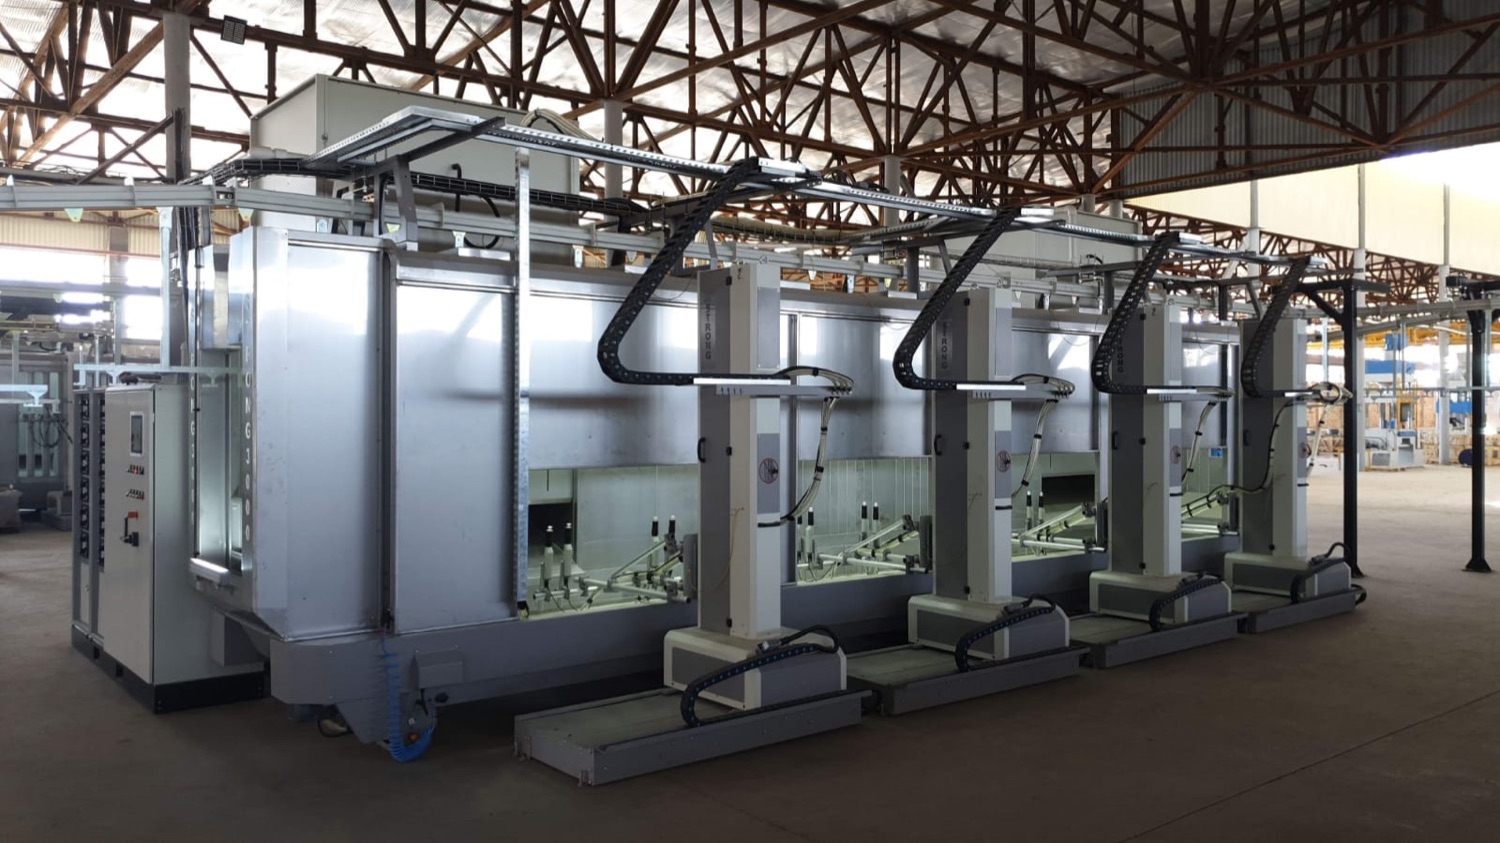
Deep-part (cavity) powder enamel system: overhead conveyor, booth, automatic gun reciprocators and control cabinet
Automatic · Deep parts

Deep-Part (Cavity) Enameling System

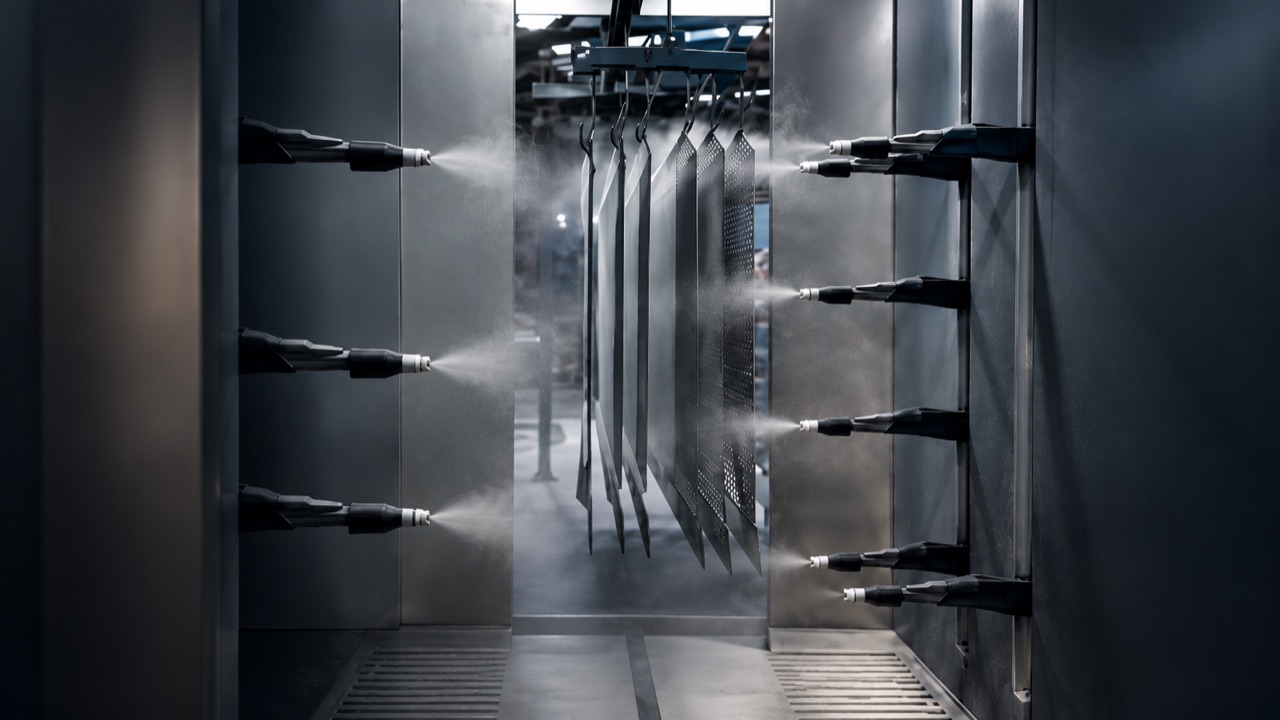
An automatic powder enamel system for deep parts such as oven cavities. Parts pass through the booth on an overhead conveyor while automatic gun reciprocators apply the enamel.

  • Application by automatic gun reciprocators
  • Parts are carried on an overhead conveyor
  • Operated from the control cabinet
Process Flow

Every Stage, Engineered for Firing.

Pretreatment
PretreatmentDegreasing & cleaning
Drying
DryingMoisture removal
Application
ApplicationEnamel powder
Recovery
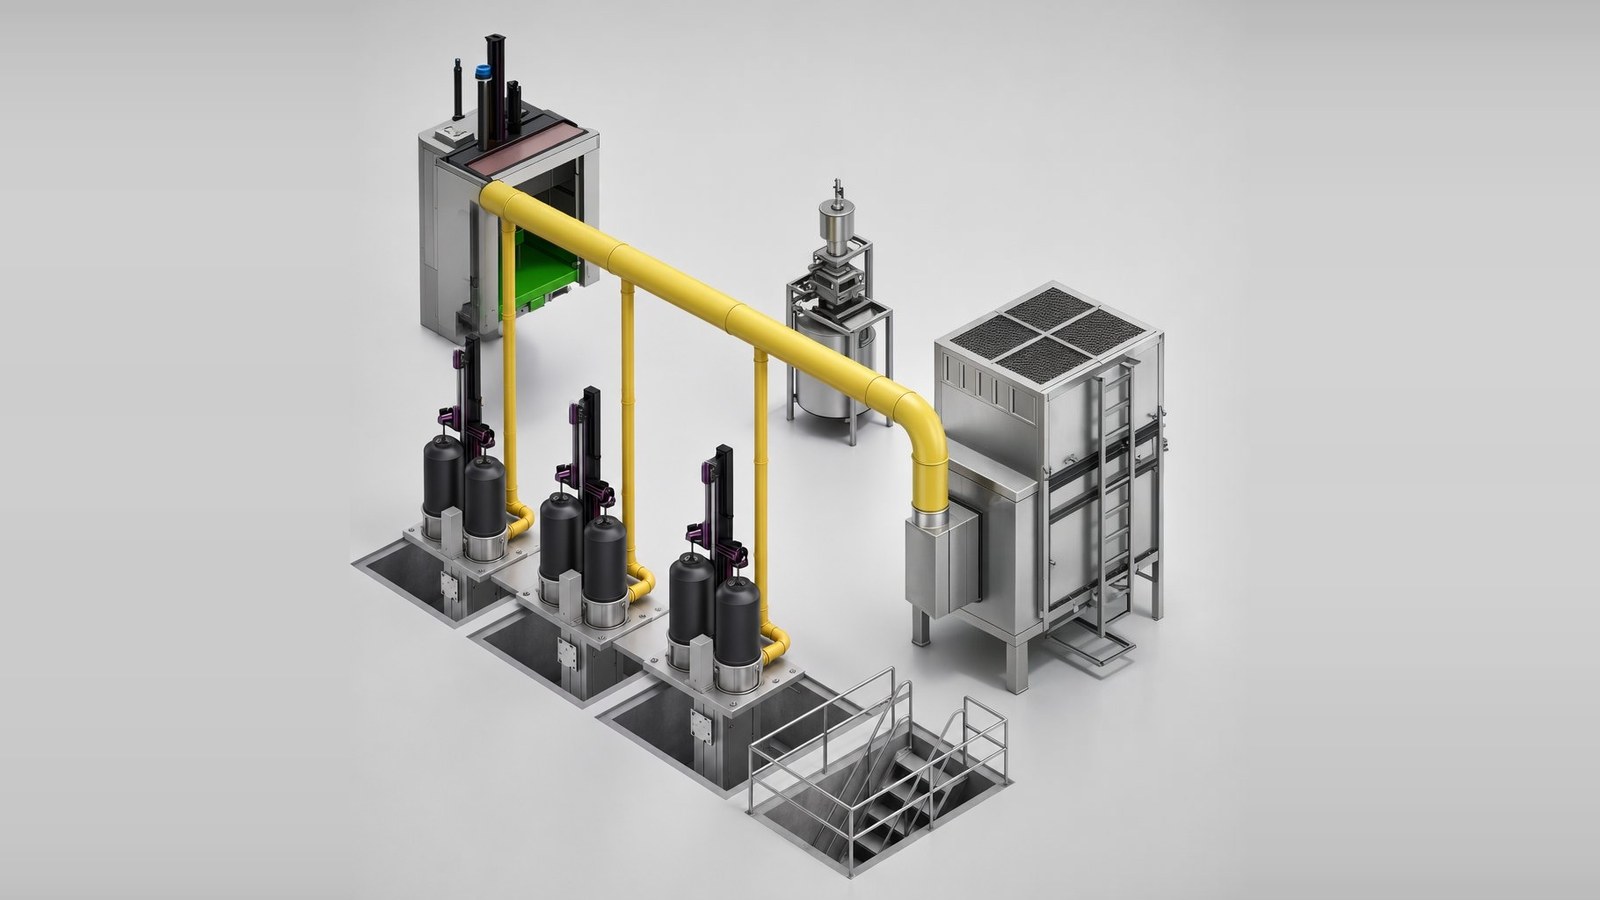
RecoveryPowder recovery
Firing
FiringHigh temperature
Automation
AutomationControl & conveying
Pretreatment · Washing

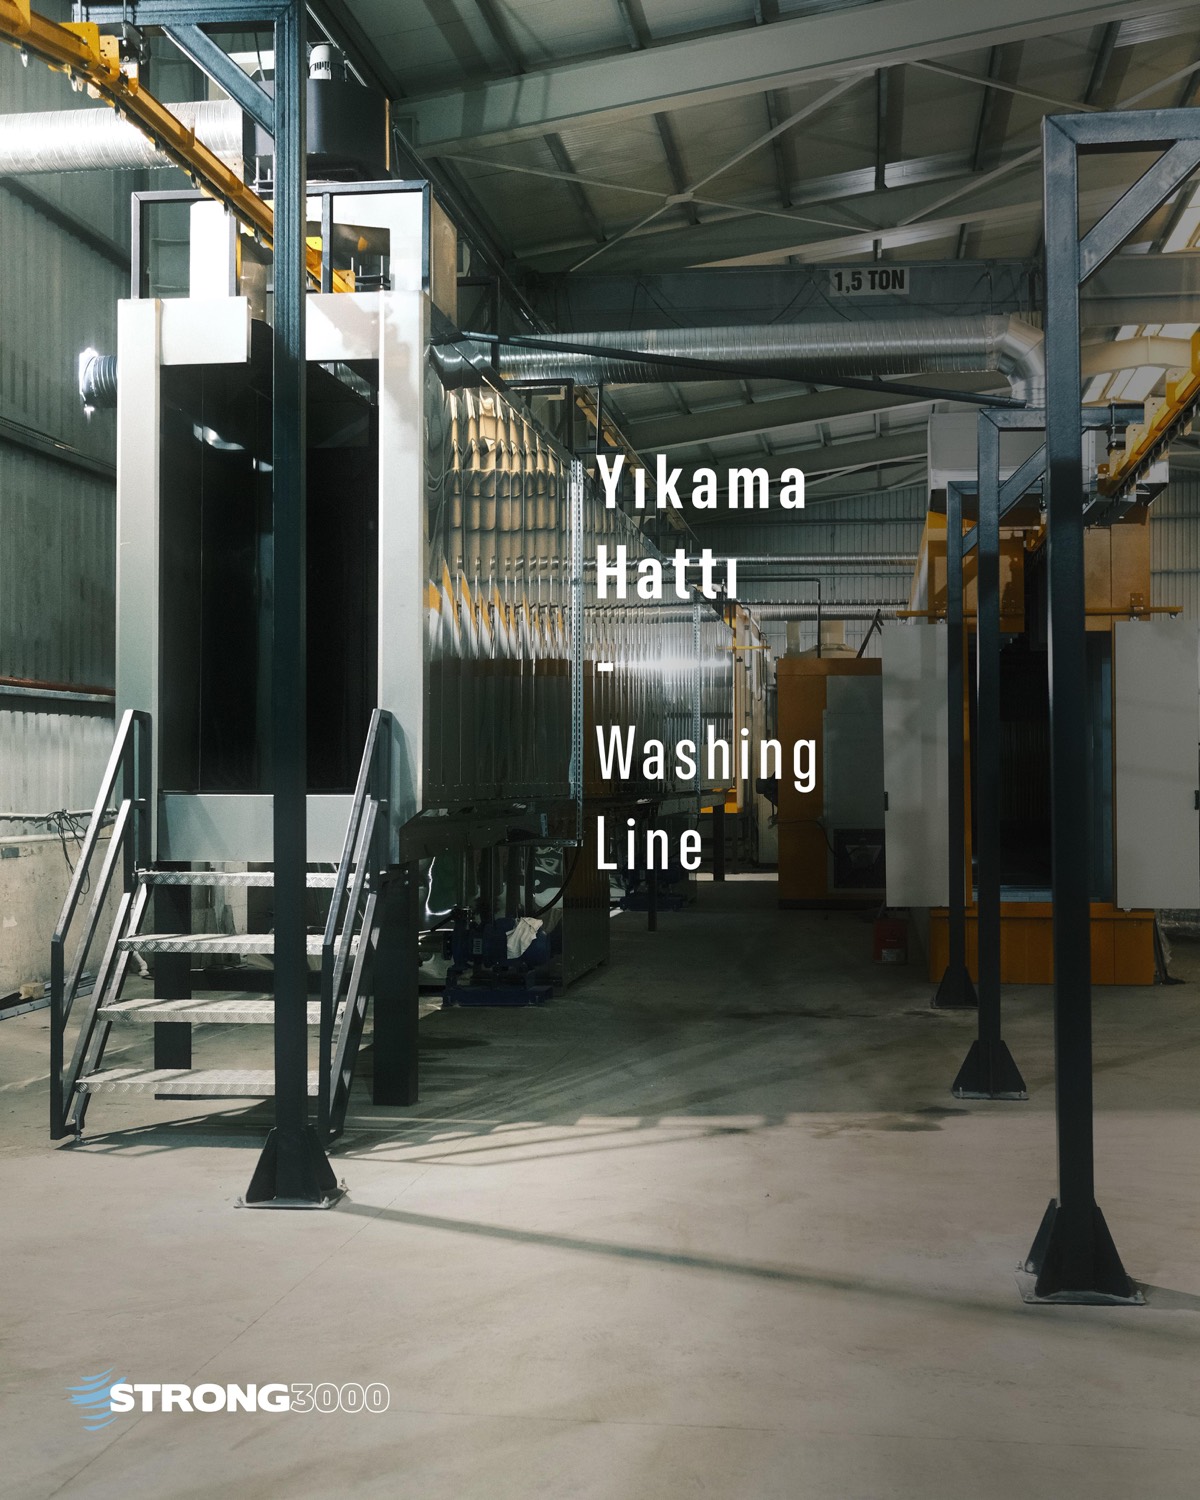
Multi-Stage Washing Line.

Surface preparation before enameling is carried out with a spray (tunnel) or dip washing line consisting of degreasing and rinsing stages. A surface free of oil and dirt is the foundation for the enamel to fuse properly to the steel.

Washing Line Models
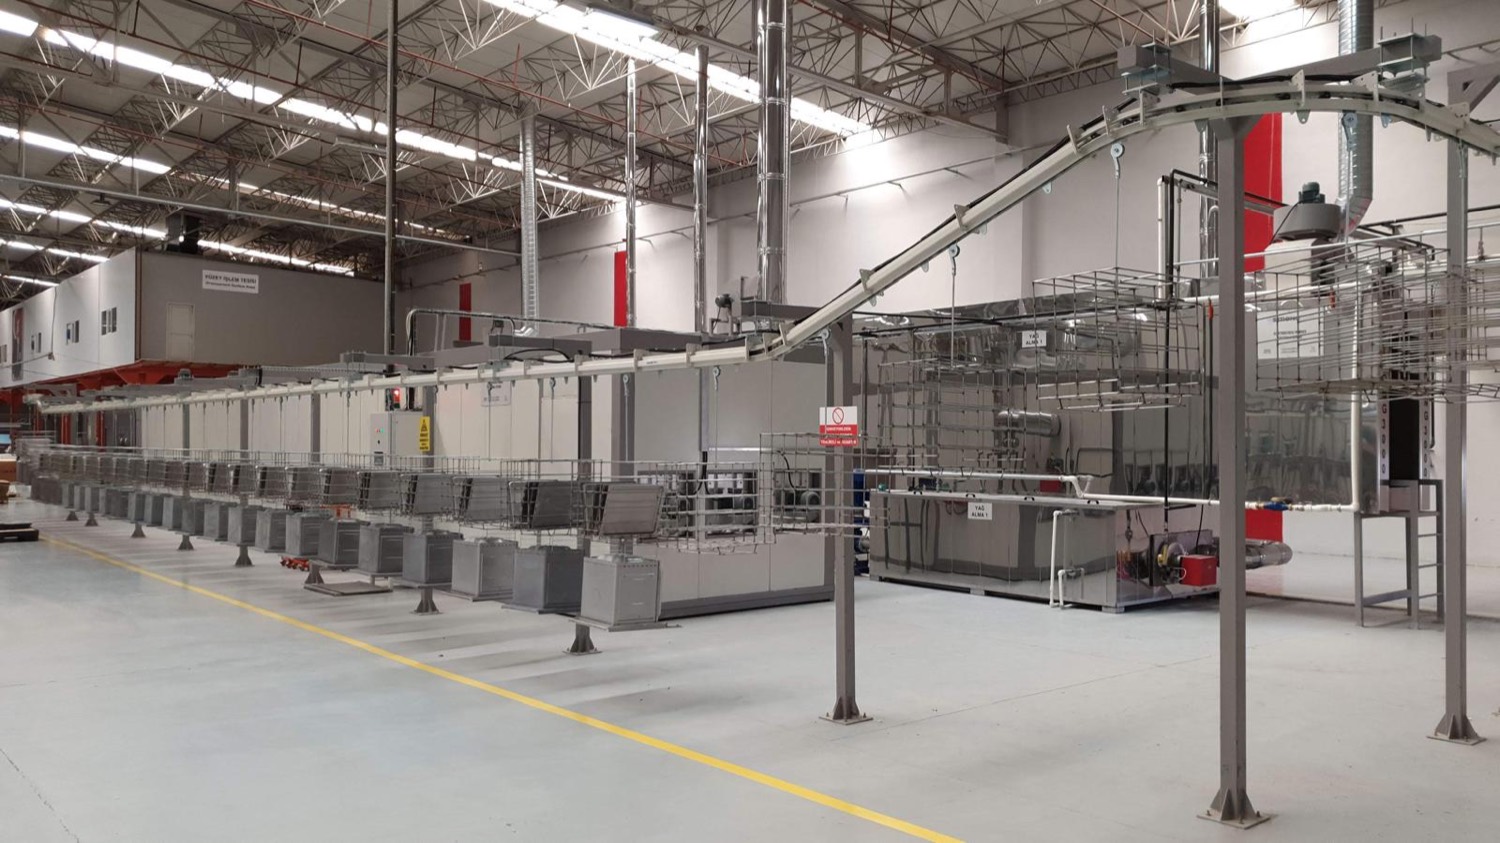
Spray-type washing line: baskets on the conveyor and the washing tunnel
Conveyorized · Tunnel

Spray-Type Washing Line

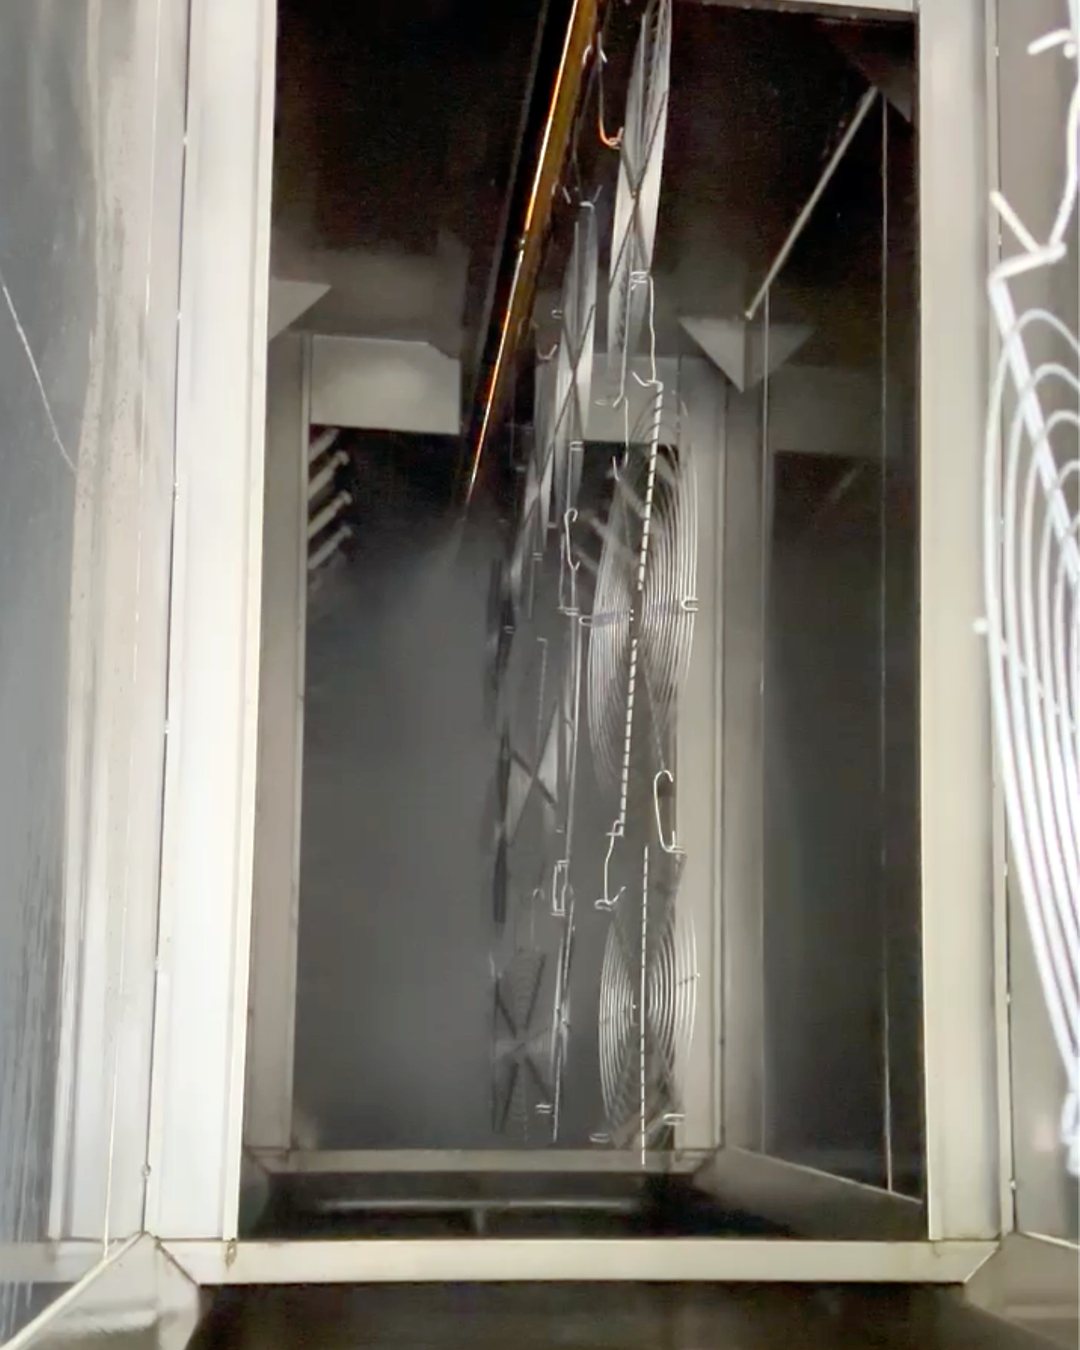
As parts travel through the tunnel on the conveyor, degreasing and rinsing solutions are sprayed through pressurized nozzles at each stage. The continuous flow gives repeatable surface preparation in series production.

  • Staged degreasing and rinsing
  • Spraying through pressurized nozzles
  • Number of stages and tunnel length to suit the part
STRONG3000 — Dry-off Oven
Drying · Moisture Removal

Drying Before Enameling

After washing, parts are freed of moisture in a dry-off oven before the enamel is applied. Because water left on the surface directly affects how the enamel powder adheres and the surface quality after firing, drying is sized to the part geometry and line speed.

Ovens · Enamel Firing

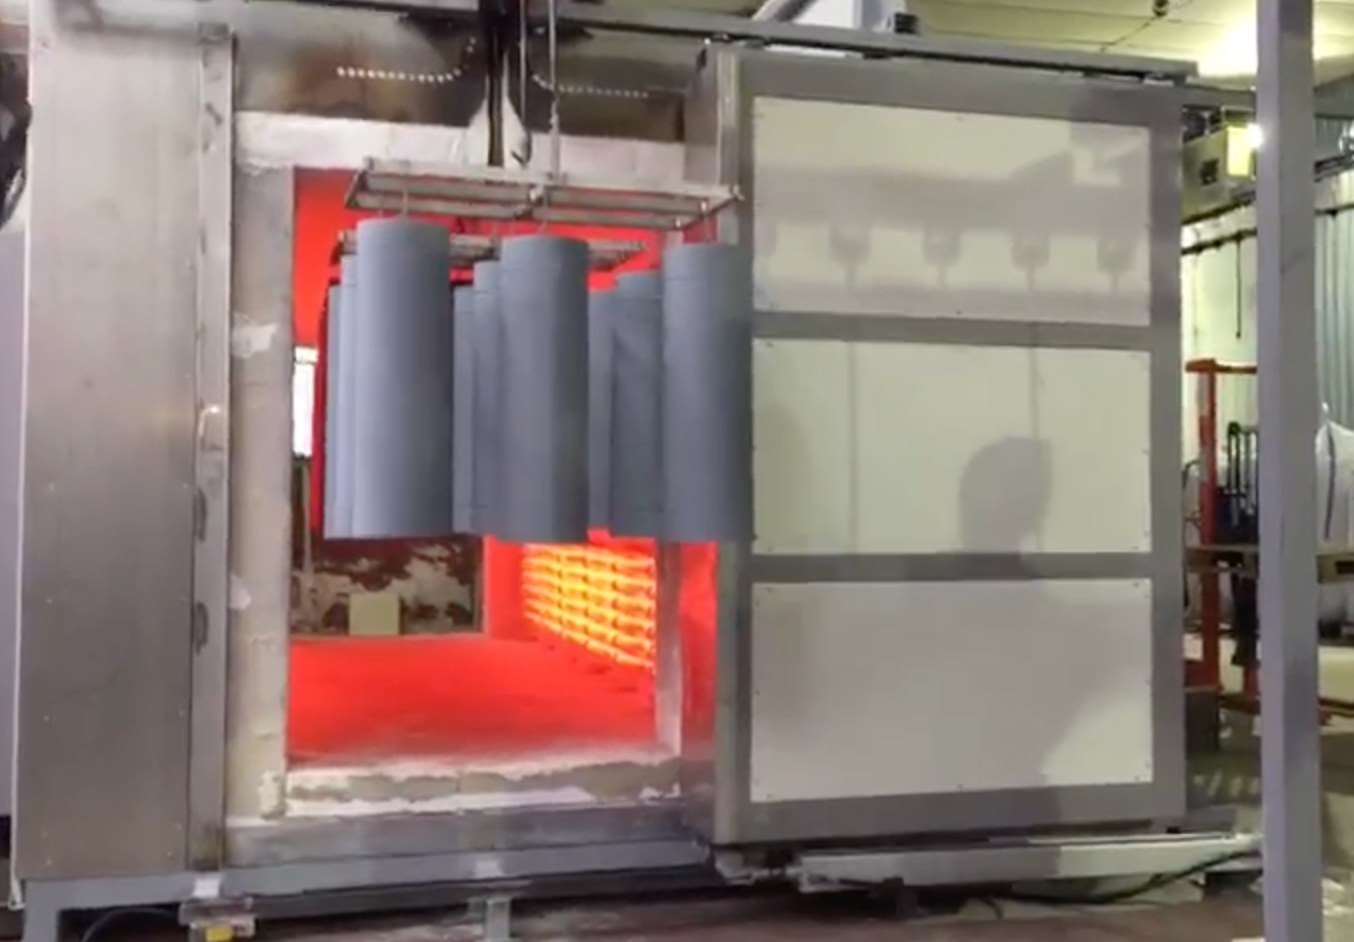
Enamel Firing Ovens.

The enamel powder (glass frit) is fired at about 780–850°C to fuse it to the steel. Ovens are sized to the part load and line speed, with gas or electric heating.

Oven Types
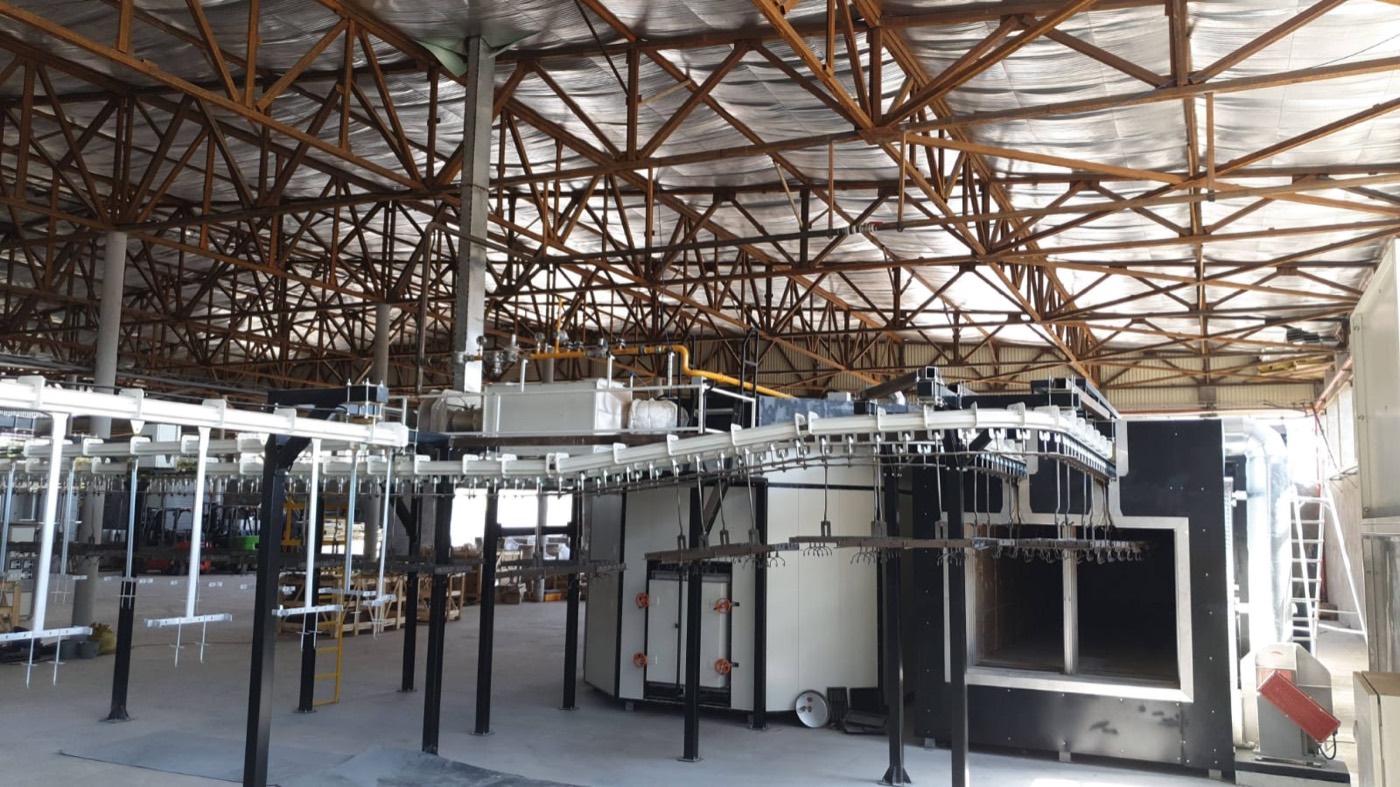
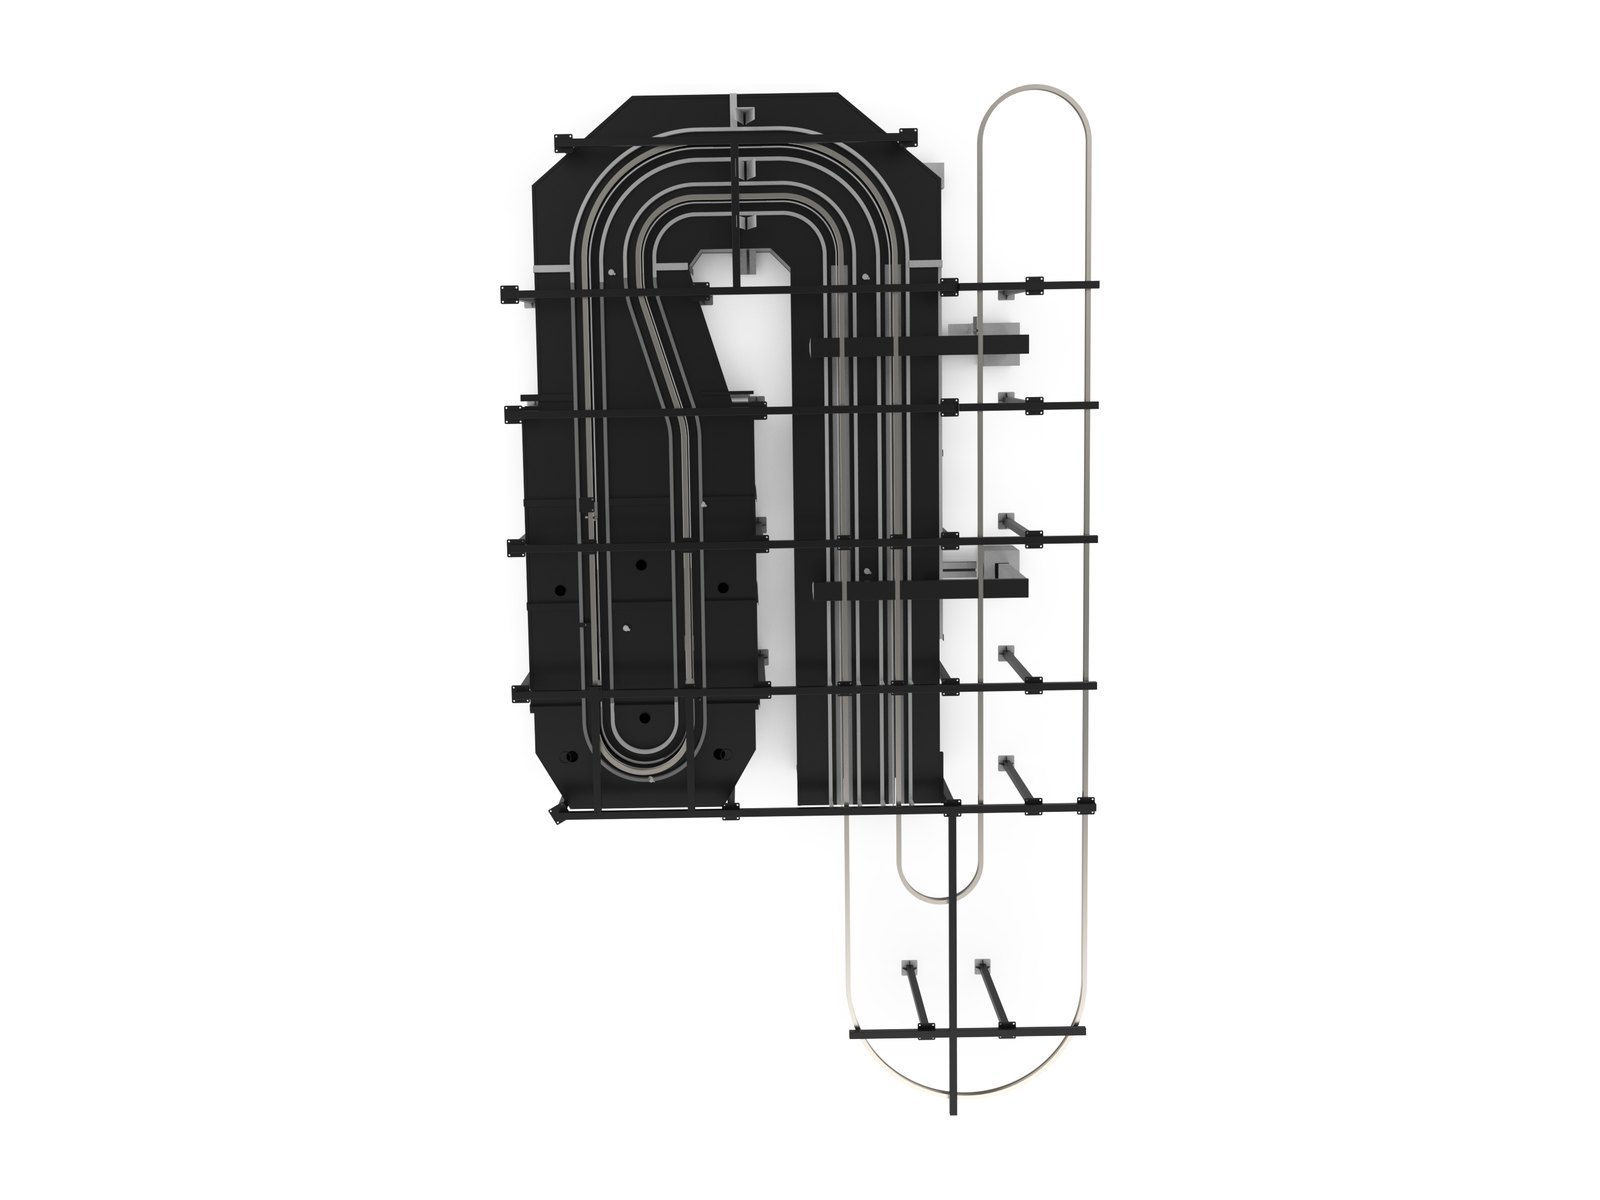
U-type enamel oven: entry and exit openings on the same side, with the overhead conveyor
U-turn conveyor

U-Type Enamel Oven

The conveyor makes a U-turn inside the oven, so the entry and exit are on the same side. It takes up less floor space than a long straight tunnel.

  • Entry and exit on the same side
  • Less floor space than a straight tunnel
  • Continuous firing on the conveyor
Option

Climate Room.

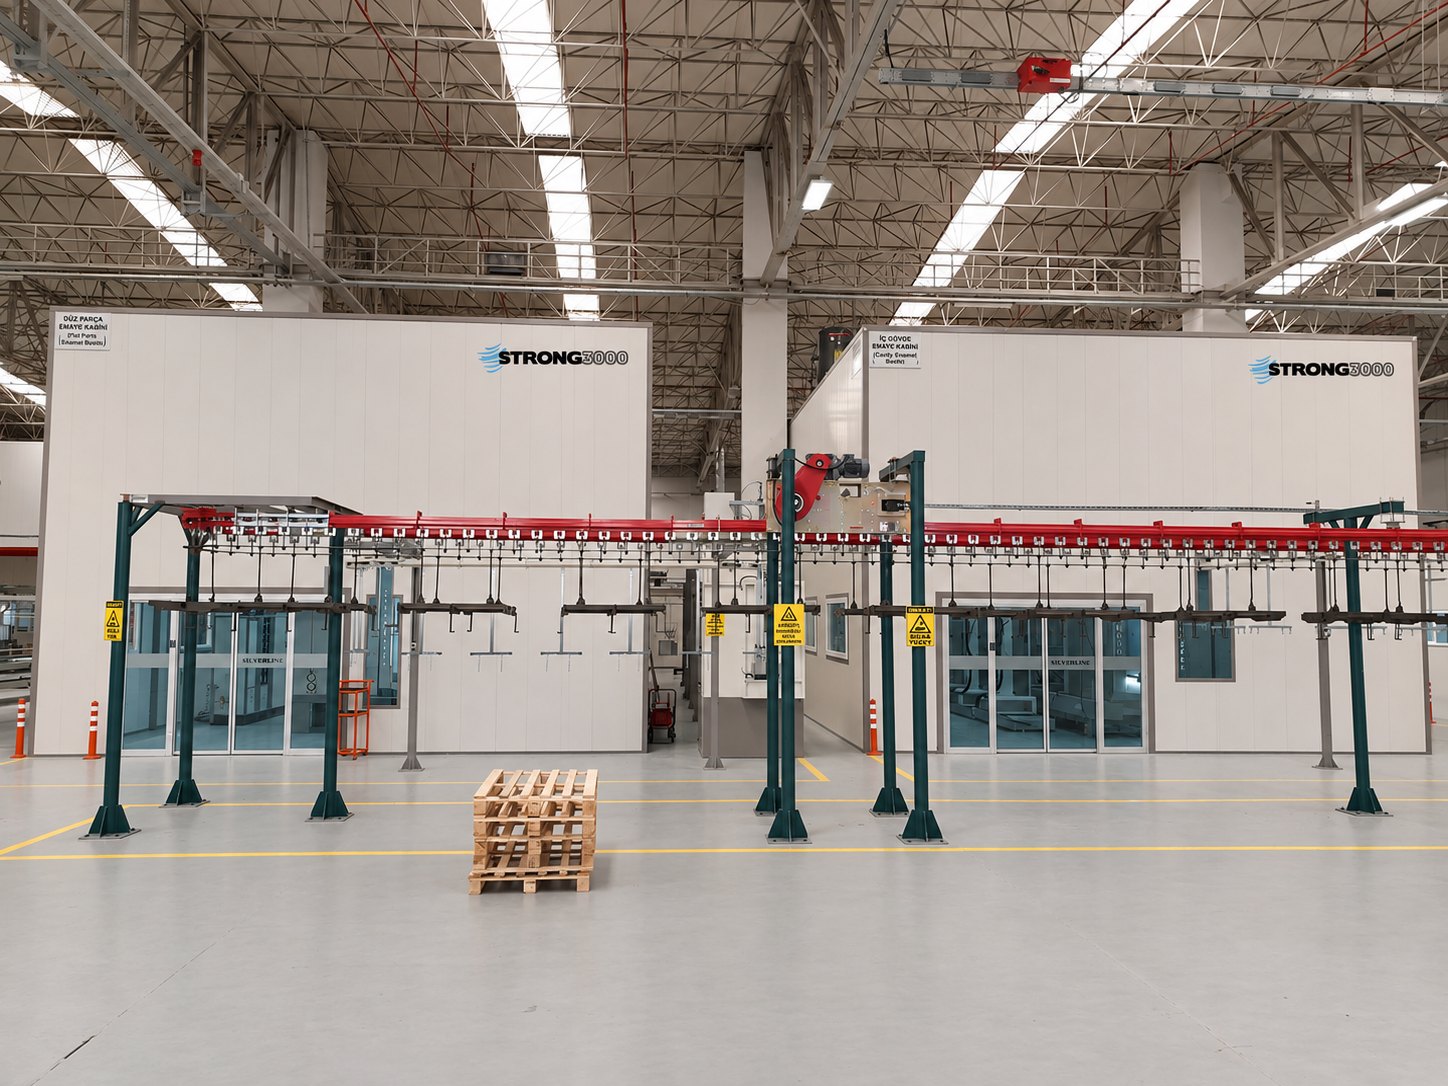
If required, the application area is enclosed in an insulated room with controlled temperature and humidity, so coating conditions stay stable regardless of the season.

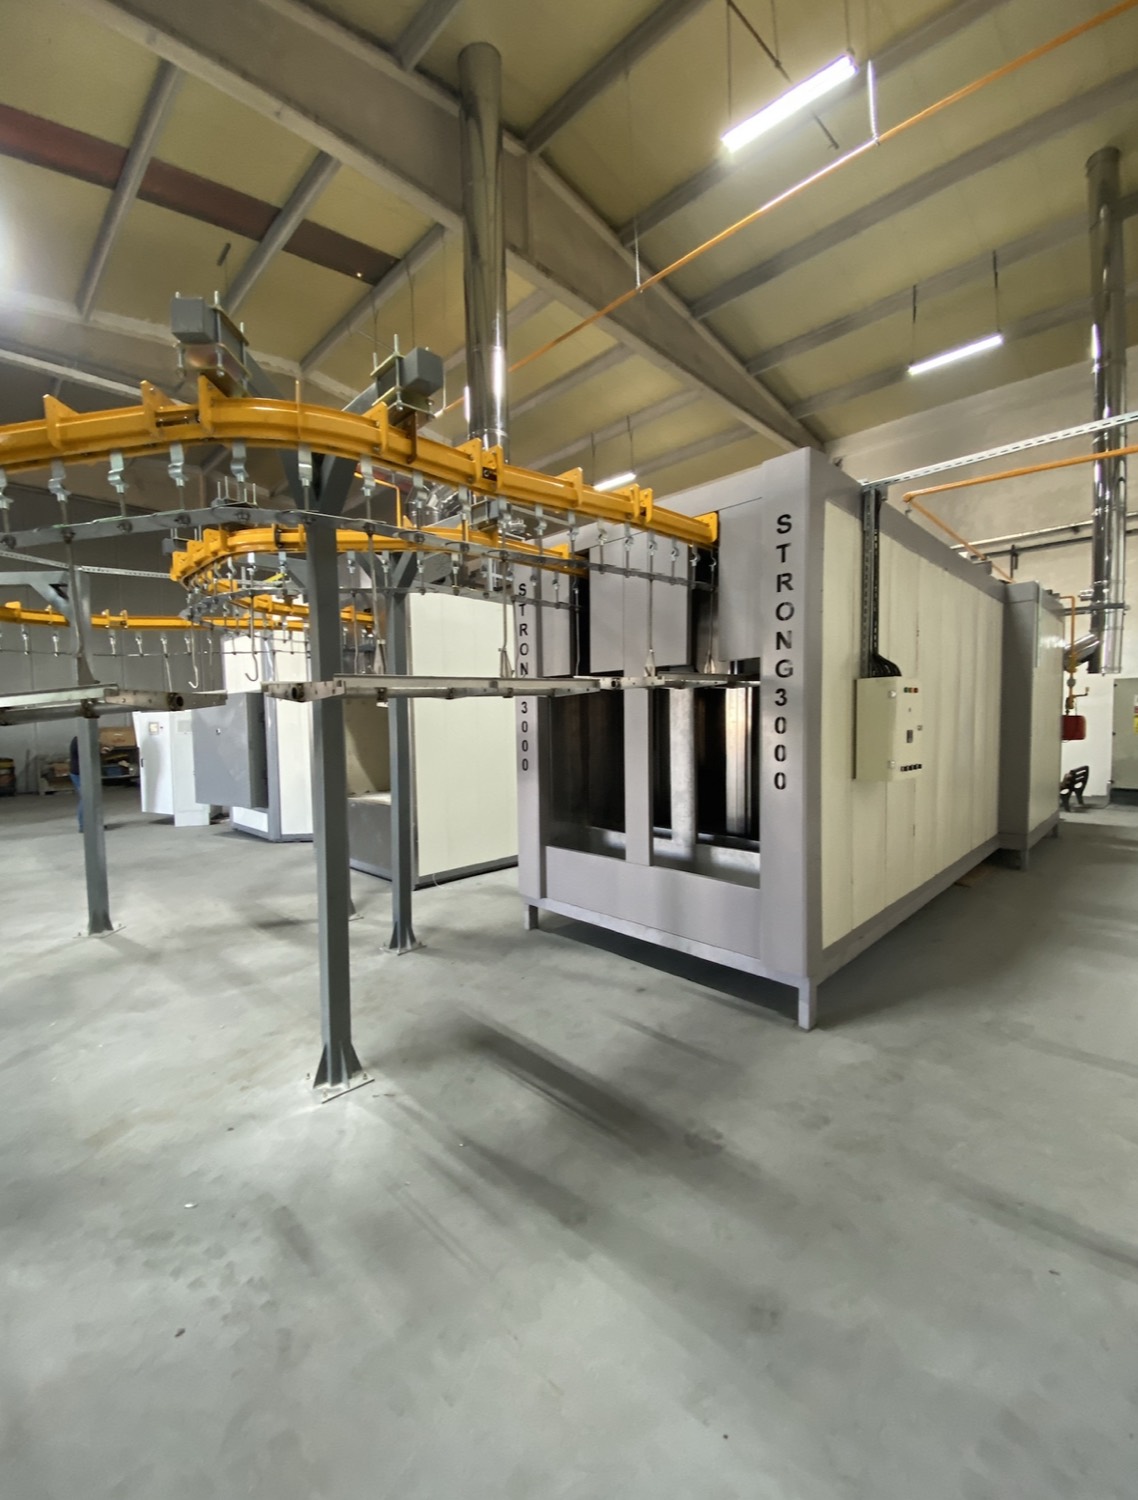
Two STRONG3000 climate rooms side by side with the overhead conveyor
Temperature · Humidity control

Controlled Application Environment

Panel construction, climate control and air circulation keep the application zone under stable conditions. The room is planned together with the booth and application equipment.

  • Temperature and humidity control
  • Insulated panel construction
  • Filtered air supply
Engineering & Manufacturing

Designed. Engineered.
Manufactured. Under One Roof.

STRONG3000 combines mechanical and electrical engineering, automation, control software and application technology in a single organization — so responsibility for the whole line stays in one place.

Mechanical Engineering

Booths, conveyors, ovens and recovery hardware.

Electrical Engineering

Power, control cabinets and line wiring.

Automation

Reciprocators, robotics and PLC control.

Control Software

Smart AI platform and line integration.

Application Technology

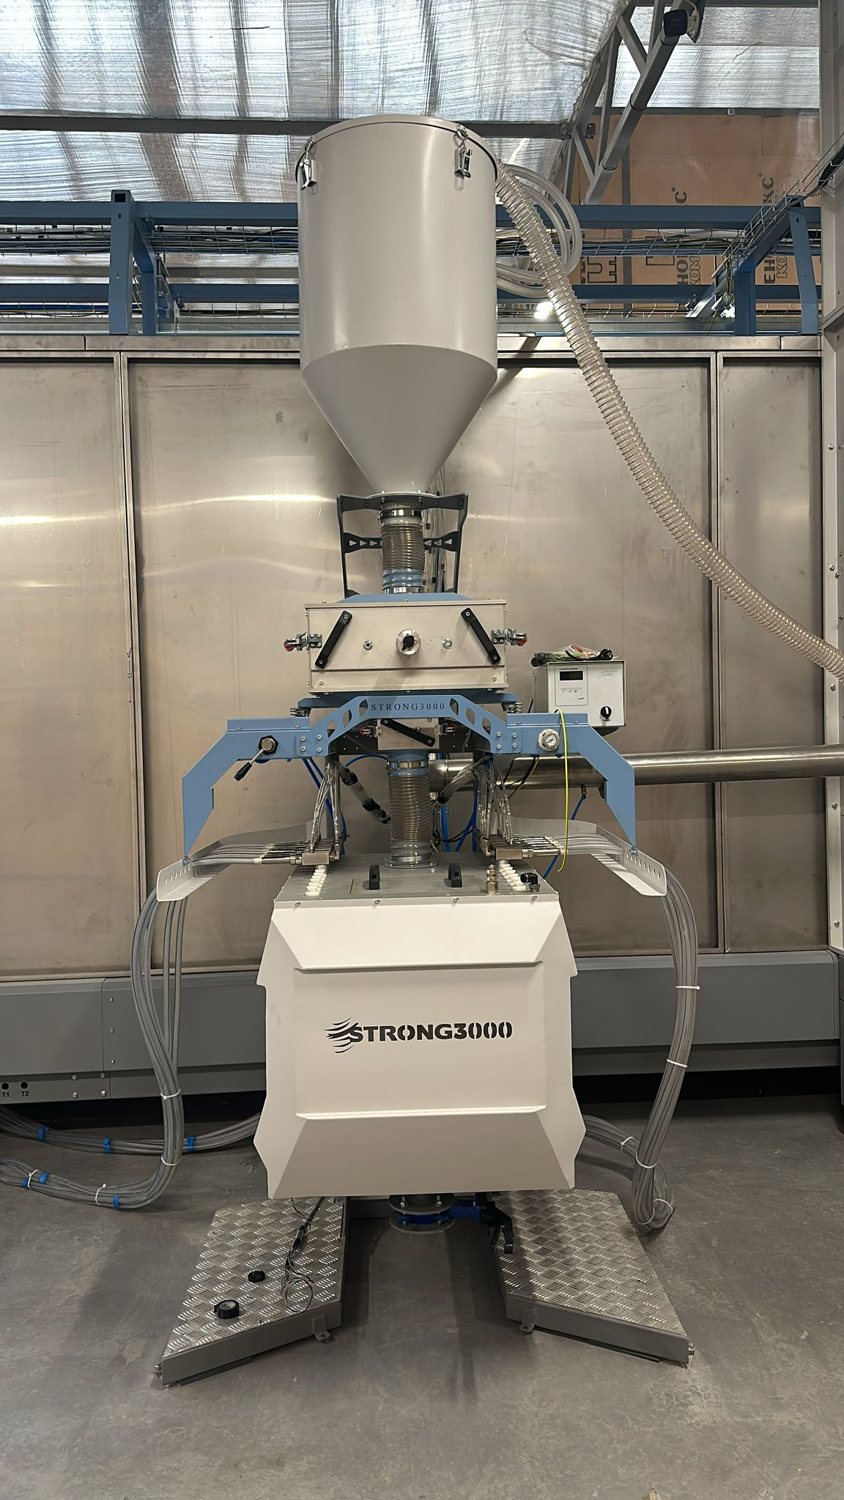
Gun, injector and powder delivery development.

FAT & Commissioning

Factory acceptance testing and on-site start-up.

Video

See It in Action.

Powder Enamel Systems — Promotional Film — video cover1:52
Powder Enamel Systems — Promotional FilmWatch on YouTube ↗
Deep-Part (Cavity) Powder Enamel Booths — video cover2:13
Deep-Part (Cavity) Powder Enamel BoothsWatch on YouTube ↗
Enamel Firing Oven Line — video cover0:51
Enamel Firing Oven LineWatch on YouTube ↗
Case Studies

Enamel in Production.

STRONG3000 — Cavity Powder Enamel Plant
Powder EnamelCavity

Powder Enamel Cavity Coating Plant with Climate Room

An electrostatic powder enamel coating plant with a climate room for cavity (oven interior) parts.

Project No.0472
STRONG3000 — Cavity Powder Enamel Plant
Powder Enamel

Cavity Powder Enamel Plant

A powder enamel coating plant project for cavity parts.

Project No.1356
STRONG3000 — Automated Flat Part Enameling Plant
Powder EnamelAutomation

Automated Flat Part Enameling Plant

Automated enamel application and material handling plant for flat parts.

Project No.1338
See all case studies
Documentation

Technical Datasheet & Documents.
Turnkey Powder Enameling Lines — Technical Datasheet
PDF · All the technical content of this page
Download
Talk to an Engineer

Planning a Powder Enameling Line?

Discuss your part, firing requirements and capacity directly with STRONG3000's engineering team.

Powder Coating Lines