In Short
- For decorative work, the target is generally 60–80 µm; where there is chemical/mechanical load, the 60–90 µm band is used.
- Thickness is measured not on the wet film but on the cured dry film (DFT); a magnetic probe is used on steel and an eddy current probe on aluminum.
- Too little thickness means weak hiding and corrosion protection; too much thickness means orange peel, sagging and cost.
- Thickness is determined by gun settings, line speed and the recovery ratio together.
The most common complaint in the field is one of these two extremes: either the part has not covered in certain areas, or the surface is wavy like orange peel. Behind both there is usually the same variable: film thickness. The micron value of a powder coating directly determines both the appearance and the protective life of the coating. Hitting the right band depends not on a single gun setting but on the powder type, part geometry and line speed.
Ideal Thickness
There is no single answer to the question “How many microns should powder coating be?”; the function decides. Still, there are workable ranges for the field. On flat, visible decorative surfaces (furniture profiles, white goods panels, architectural sheet), the target is generally between 60–80 µm. In this band, hiding is sufficient, the surface keeps its flow and the risk of orange peel stays low.
For outdoor work, humid environments or jobs with a light chemical load, it is common to push the band up slightly to the 60–90 µm range. Functional differences come into play here: if corrosion protection is the priority, you raise the lower limit; if a fine, smooth surface is wanted, you do not push the upper limit.
- Decorative flat surface: flow and appearance first, 60–80 µm.
- Exterior facade / architectural polyester: UV and corrosion; most Qualicoat work requires a minimum of 60 µm.
- Functional / heavy duty: close to the upper band where there is mechanical and chemical load, while respecting the sagging limit.
Tip
Take the target thickness from the powder manufacturer’s technical datasheet (TDS). Even within the same RAL shade, hiding power varies with the formulation; dark shades cover at 60 µm while some light and metallic shades need a thicker film. The exact value is confirmed by measurement on site.
| Use / part | Target DFT (µm) | Note |
|---|---|---|
| Indoor decorative panel | 60-80 | Smooth flow, low orange peel |
| White goods / furniture profile | 60-80 | Appearance first |
| Exterior architectural (polyester) | 60-90 | Qualicoat minimum ~60 µm |
| Functional part exposed to corrosion | 80-90 | Upper band, respect the sagging limit |
| Textured (structured) powder | 70-100 | A thicker film is normal for texture |
How to Measure
Measurement gets confused between two stages: wet film and dry film. In powder coating, freshly applied electrostatic powder is still a loose layer; measuring it has little practical meaning. The real value is the dry film thickness (DFT), i.e. the hardened layer left on the part after curing. DFT is measured after curing, once the part has cooled.
The substrate determines the measuring principle:
- Magnetic (magnetic pull-off / Hall) probe: on a ferromagnetic substrate, i.e. steel. The instrument reads coating thickness from the weakening of the magnetic field between the probe and the metal.
- Eddy current probe: on non-magnetic conductive substrates such as aluminum and stainless steel. Thickness is calculated from the change in the eddy current induced in the surface.
Most modern DFT gauges combine both principles in a single probe and recognize the substrate automatically. For a correct reading, the gauge must be zeroed on the bare substrate to be measured and verified with a calibration foil of known thickness. Do not take the measurement from a single point; take it from the flat central area of the part, from the edges and, if present, from recesses/corners. DFT varies significantly even across a single part; the lowest value matters as much as the average.
Caution
Measure 1–2 cm in from the edge. Near edges and outer corners, the film both settles thinner and the probe may read incorrectly. Edge coverage is a separate issue; do not assess it with a single reading.
Low Thickness Problems
When the film falls below target, the first sign is poor hiding. The color of the underlying surface or the metallic sheen shows through the film; this is called show-through. Especially when applying a light shade over steel, shade shift and a mottled appearance often appear in the 40–50 µm band.
- Poor hiding: a thin film cannot fully cover the substrate; a light shade over a dark substrate is the most critical case.
- Poor corrosion protection: a thin film cannot form a continuous barrier. Micropores and weak edges are starting points for corrosion. In the salt spray test (ASTM B117), thin areas fail first.
- Lower mechanical strength: a very thin coating does not provide enough cushioning against scratches and impact.
A thin film often comes together with the Faraday cage effect: charged particles cannot get into inside corners, recesses and profile interiors, and these areas stay thin. The fix is to lower the gun’s kV/µA values, correct the angle and distance and, if necessary, touch up these areas manually.
Excess Thickness
Increasing thickness without limit does not improve protection; beyond a certain point it only causes problems. The most visible one is orange peel: as the film gets thicker, it becomes harder for the melted powder to flow out and level, and the surface becomes wavy. On vertical parts, excess powder runs downward as it melts and causes sagging (curtains/drips).
- Orange peel: thick film + insufficient flow; generally becomes pronounced above 120 µm.
- Sagging: excess powder buildup on vertical surfaces, running during curing.
- Edge buildup: the electrostatic charge concentrates at edges; a thick edge creates both an appearance issue and a cracking risk.
- Cost: every extra 10 µm is straight powder consumption. Running an average of 120 µm instead of an 80 µm target increases material cost by about 50%.
Excess thickness also reduces flexibility; a thick film cracks more easily on bending and impact. That is why the “the thicker the better” logic is wrong.
Thickness Control
Thickness is held not with a single knob but by balancing three variables: gun settings, line speed and recovery ratio.
Gun settings
Powder output (feed), atomizing air and electrostatic values determine the film. High kV attracts a lot of powder but makes Faraday areas harder; as output increases, the film gets thicker. On automatic lines, keeping the gun-to-part distance constant improves distribution considerably. Robot or intelligent motion gun systems reduce DFT deviation on parts with changing geometry by maintaining distance and angle.
Line speed
Conveyor speed determines how long the part spends in front of the guns. If speed increases, the film thins at the same settings; if speed drops, it thickens. If thickness is drifting, check line speed first before touching output. Speed also affects cure time, so it must be considered together with oven parameters. Without stabilizing the curing conditions, a separate topic on the oven side, thickness optimization remains incomplete.
Recovery ratio
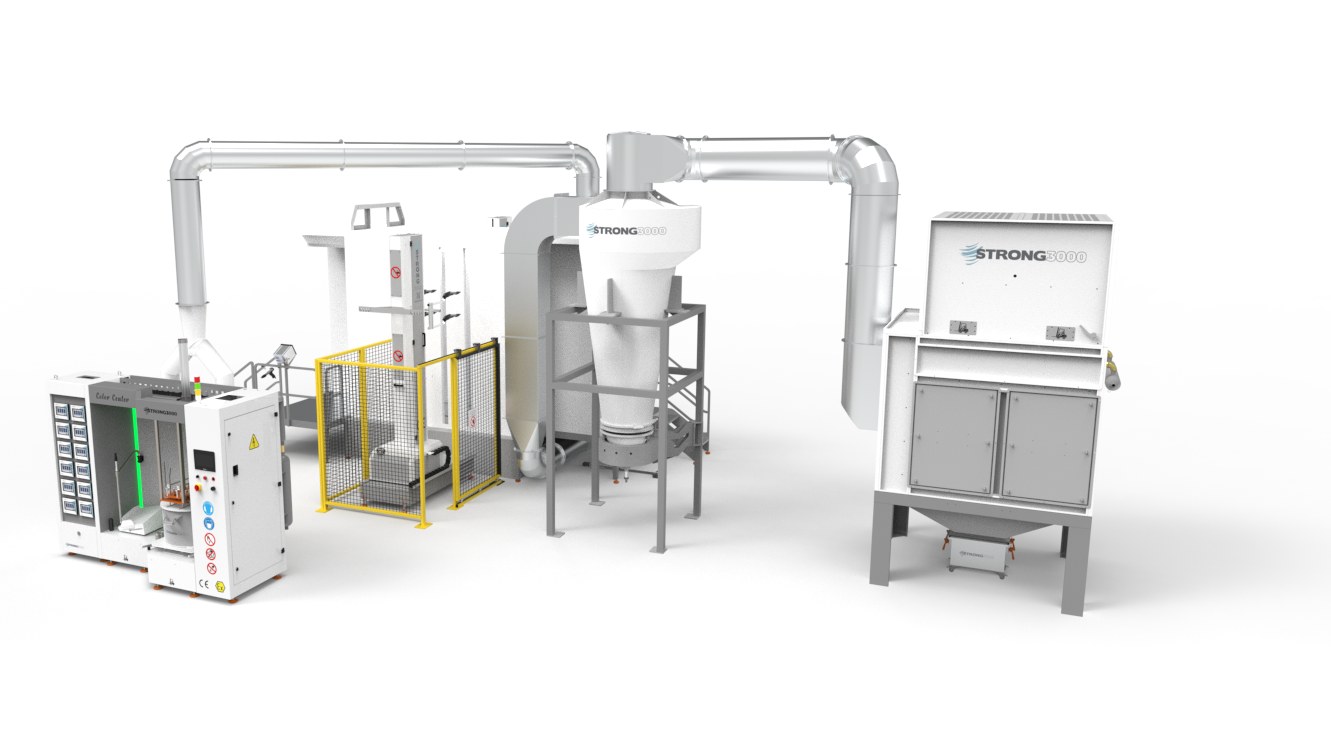
Overspray powder is collected in the recovery booth and reused blended with virgin powder. With standard powder, recovery can reach up to 95%; however, with powders high in fines below 10 µm, this drops to ~85%. The problem is this: fines accumulate in reclaimed powder. Fine powder charges differently and its flow behavior changes, which disrupts film thickness distribution. That is why reclaimed powder must be blended with virgin powder in proportion (typically 20–30%) and the buildup of fines monitored.
- If colors change frequently (3+ colors a day), a monocyclone or quick-clean booth reduces the buildup of fines and color cross-contamination.
- Cartridge/filter booths capture fine powder; when working with very fine powder, keep the feedback ratio limited.
Tip
Make DFT measurement routine: measure at least 5 points at the start of each shift and at every color/part change, and keep records. Thickness deviation usually creeps in gradually; if you catch it early, you can correct it with a single parameter (most often line speed or output).
Frequently Asked Questions
Generally 60–80 µm is targeted on decorative flat surfaces and 60–90 µm on work with corrosion or outdoor exposure. The exact value depends on the powder’s technical datasheet and the part.
Dry film thickness (DFT) is measured after curing. A magnetic probe is used on steel and an eddy current probe on non-magnetic substrates such as aluminum; the gauge is zeroed on the bare substrate and verified with a calibration foil.
As the film gets thicker, it becomes harder for the melted powder to flow out and level, and the surface becomes wavy. It generally becomes pronounced above 120 µm; it also increases the risk of sagging and edge buildup.